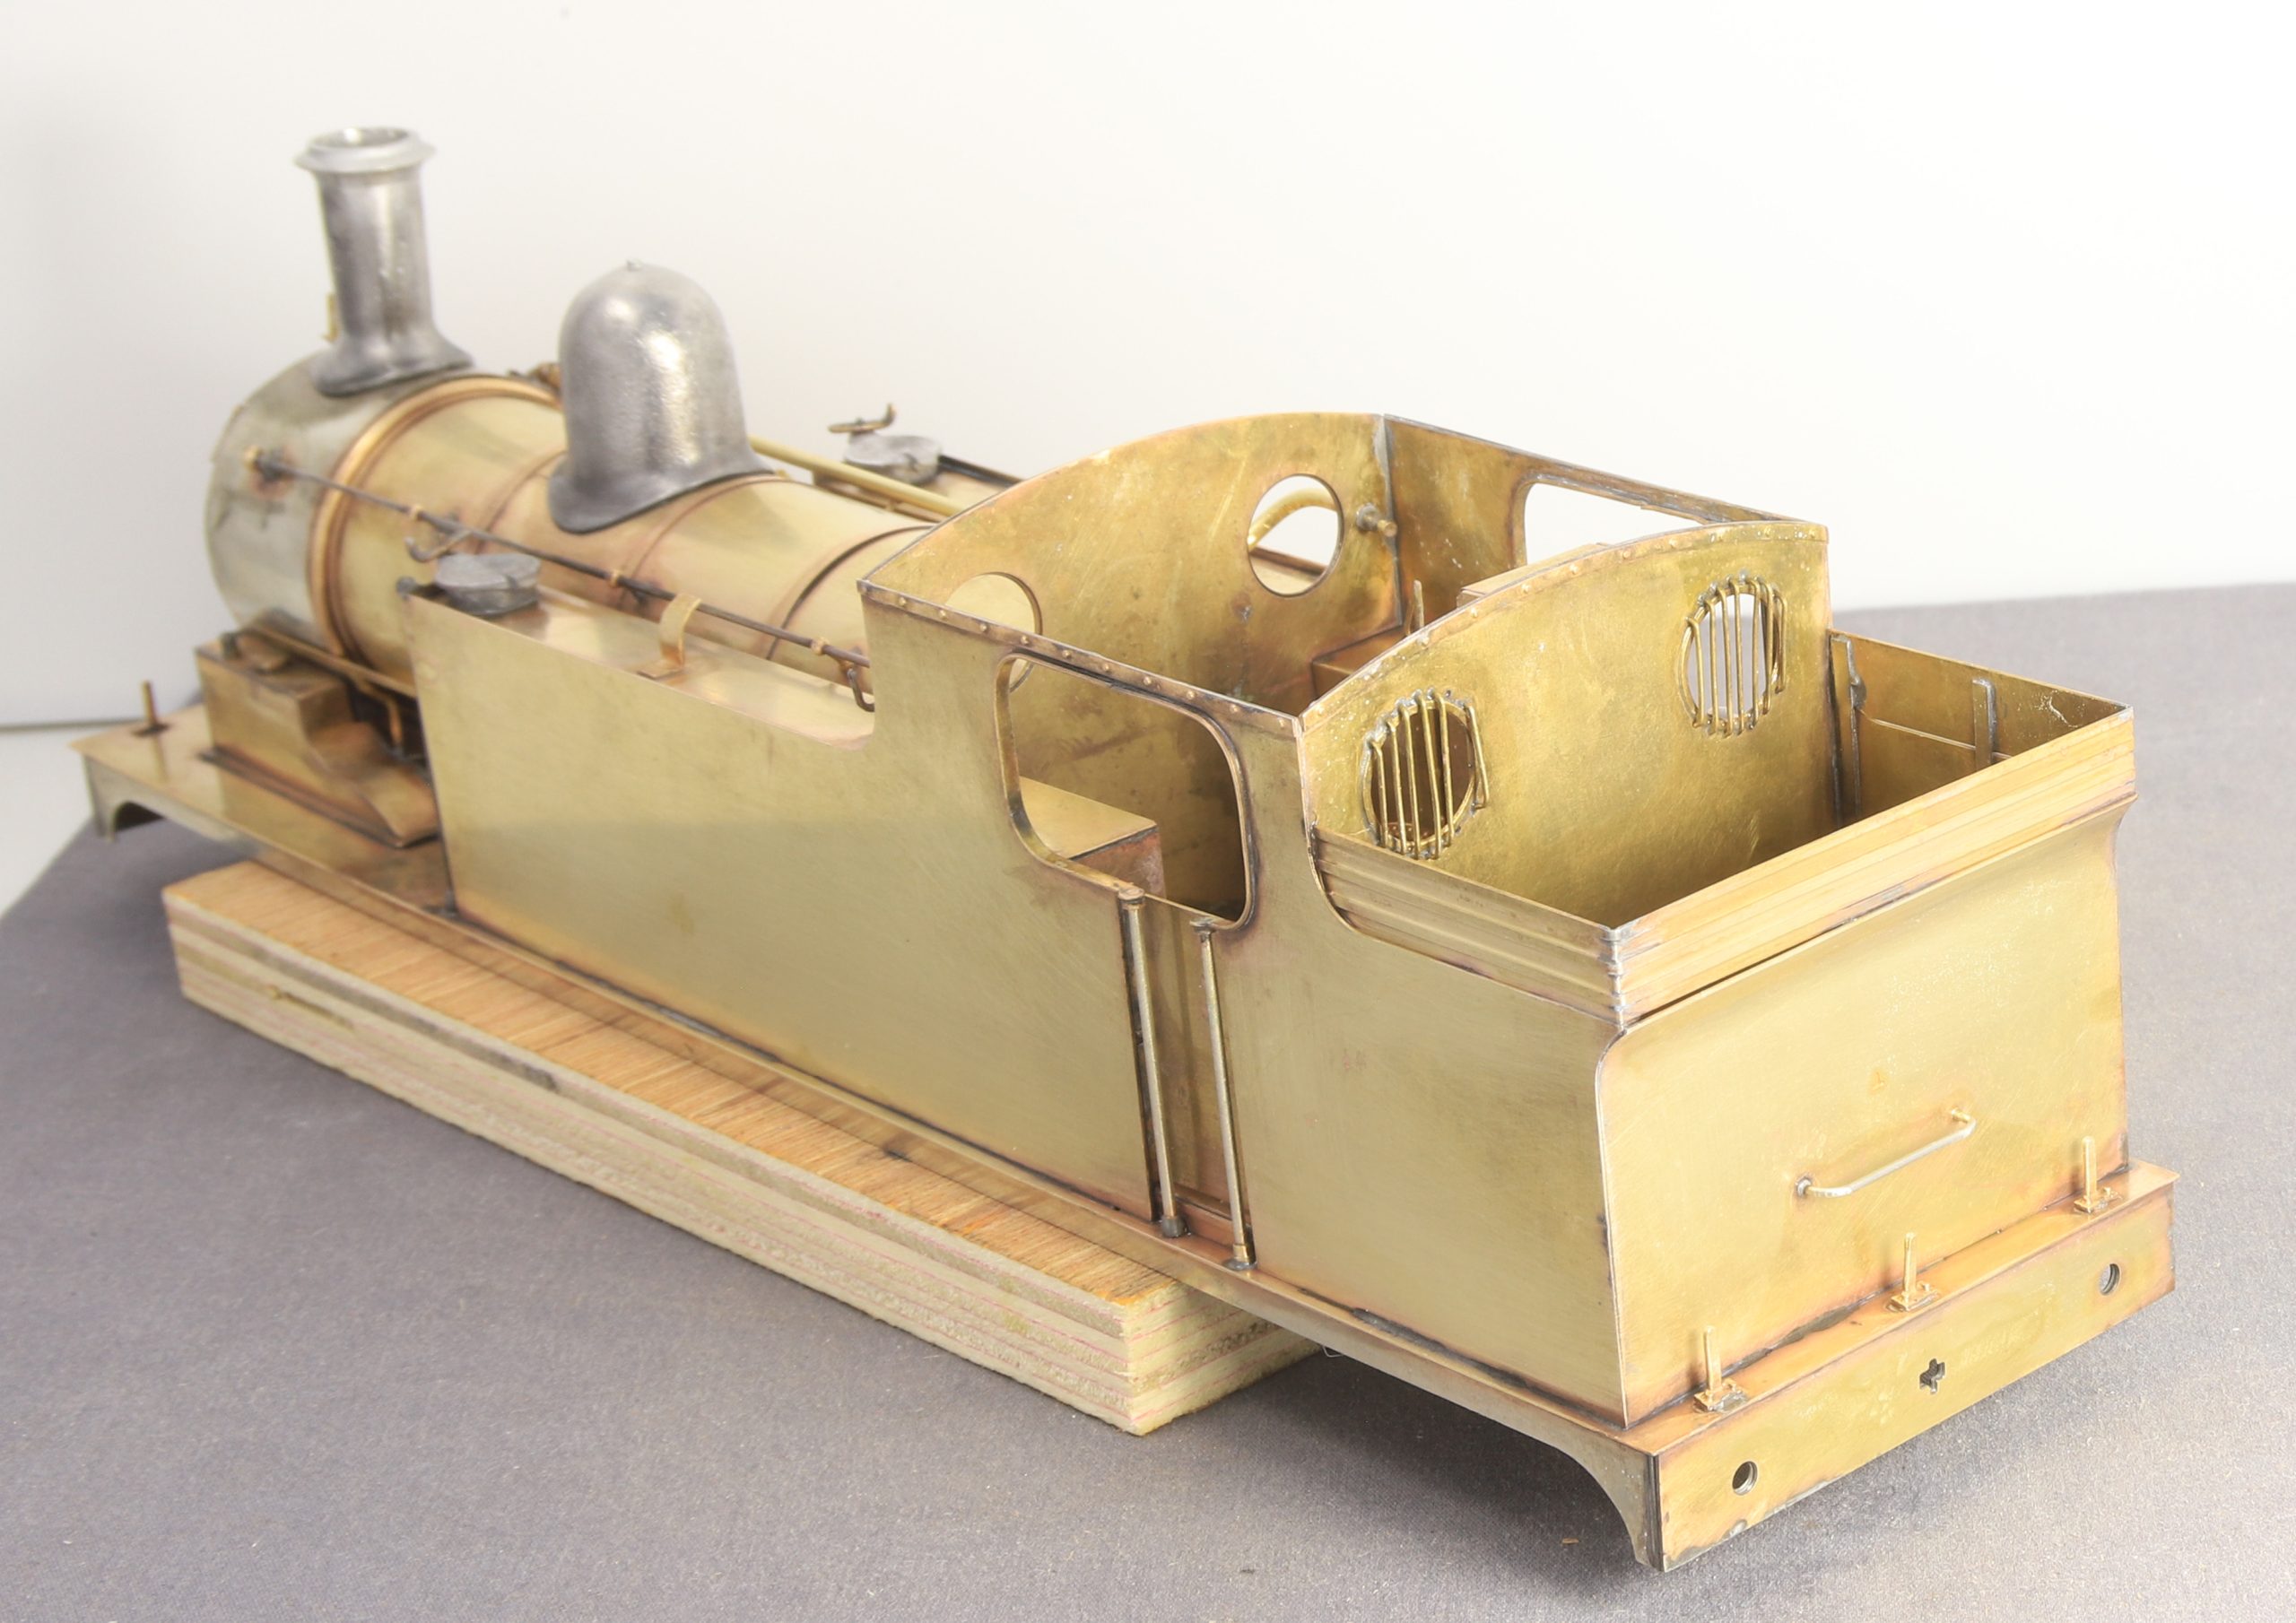
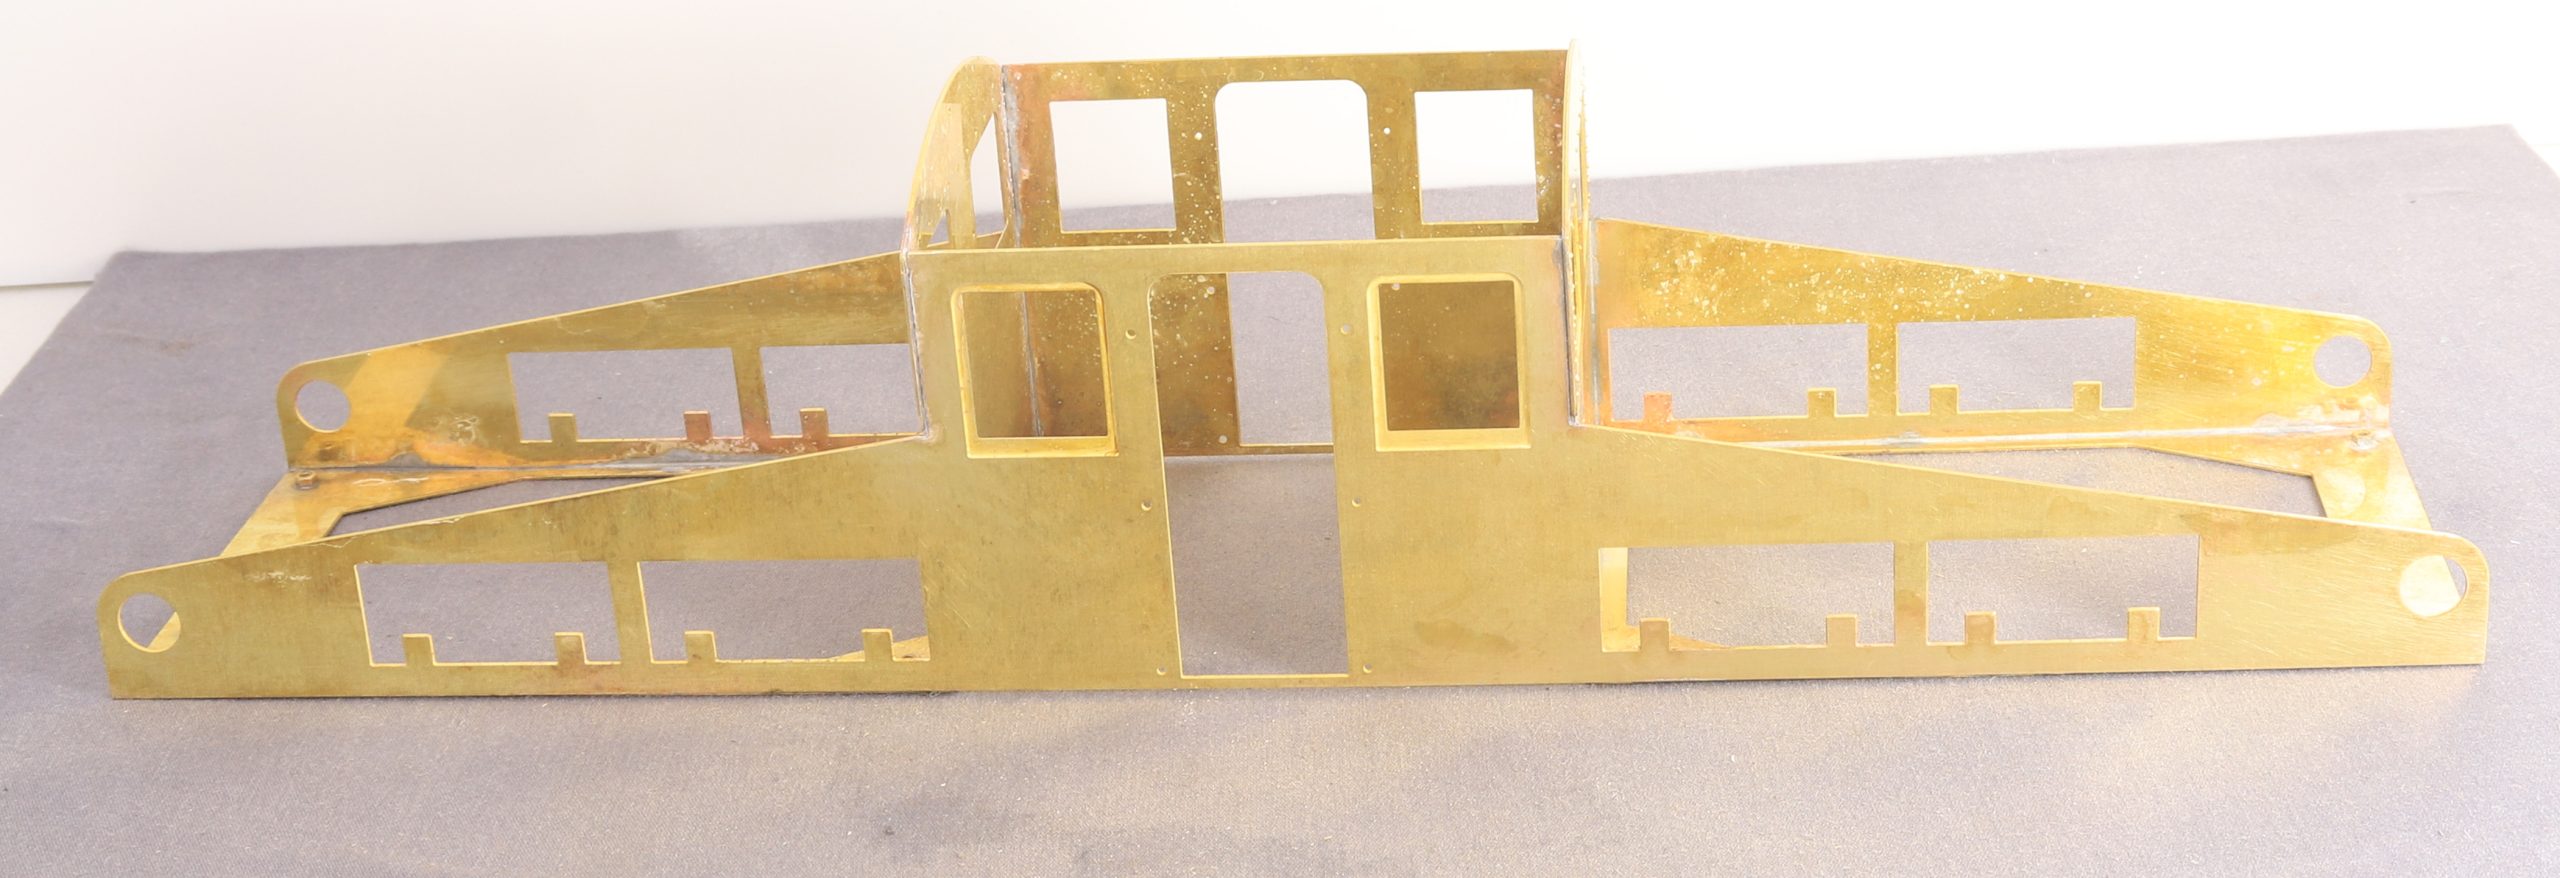
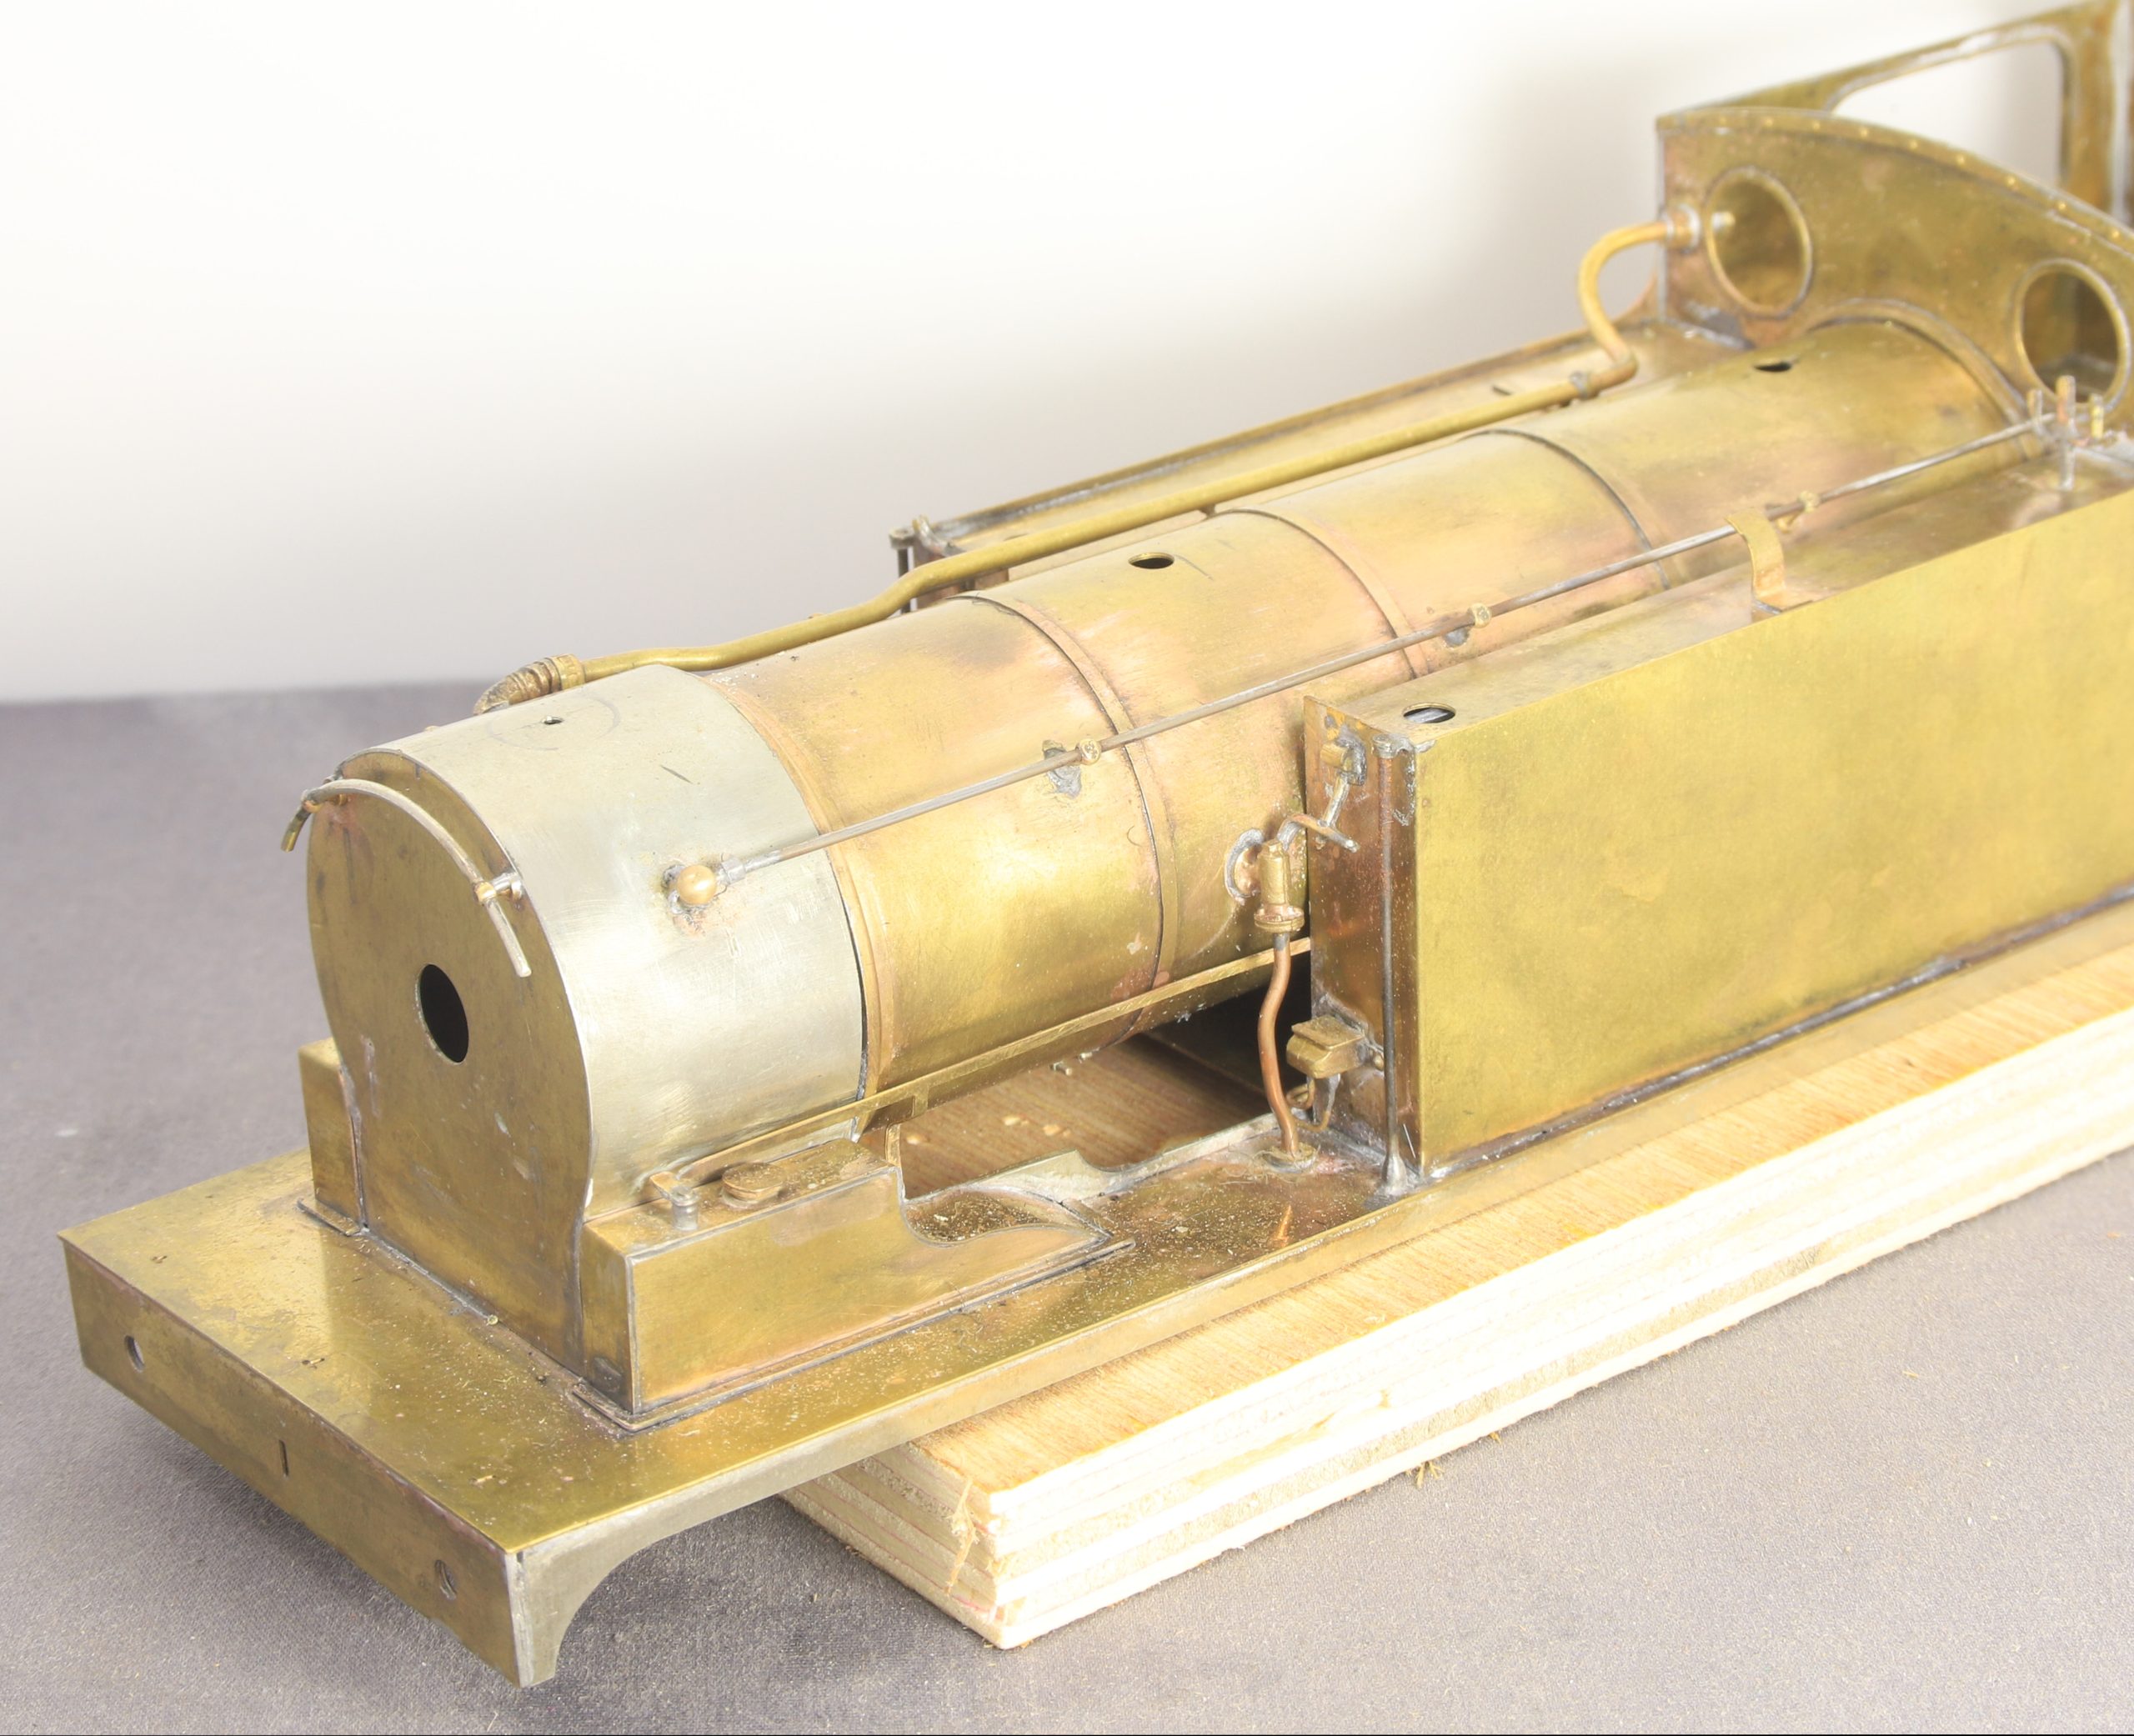
I say getting ahead of myself because I have or thought I had actually finished construction on the N10 albeit I haven’t shared photos yet.
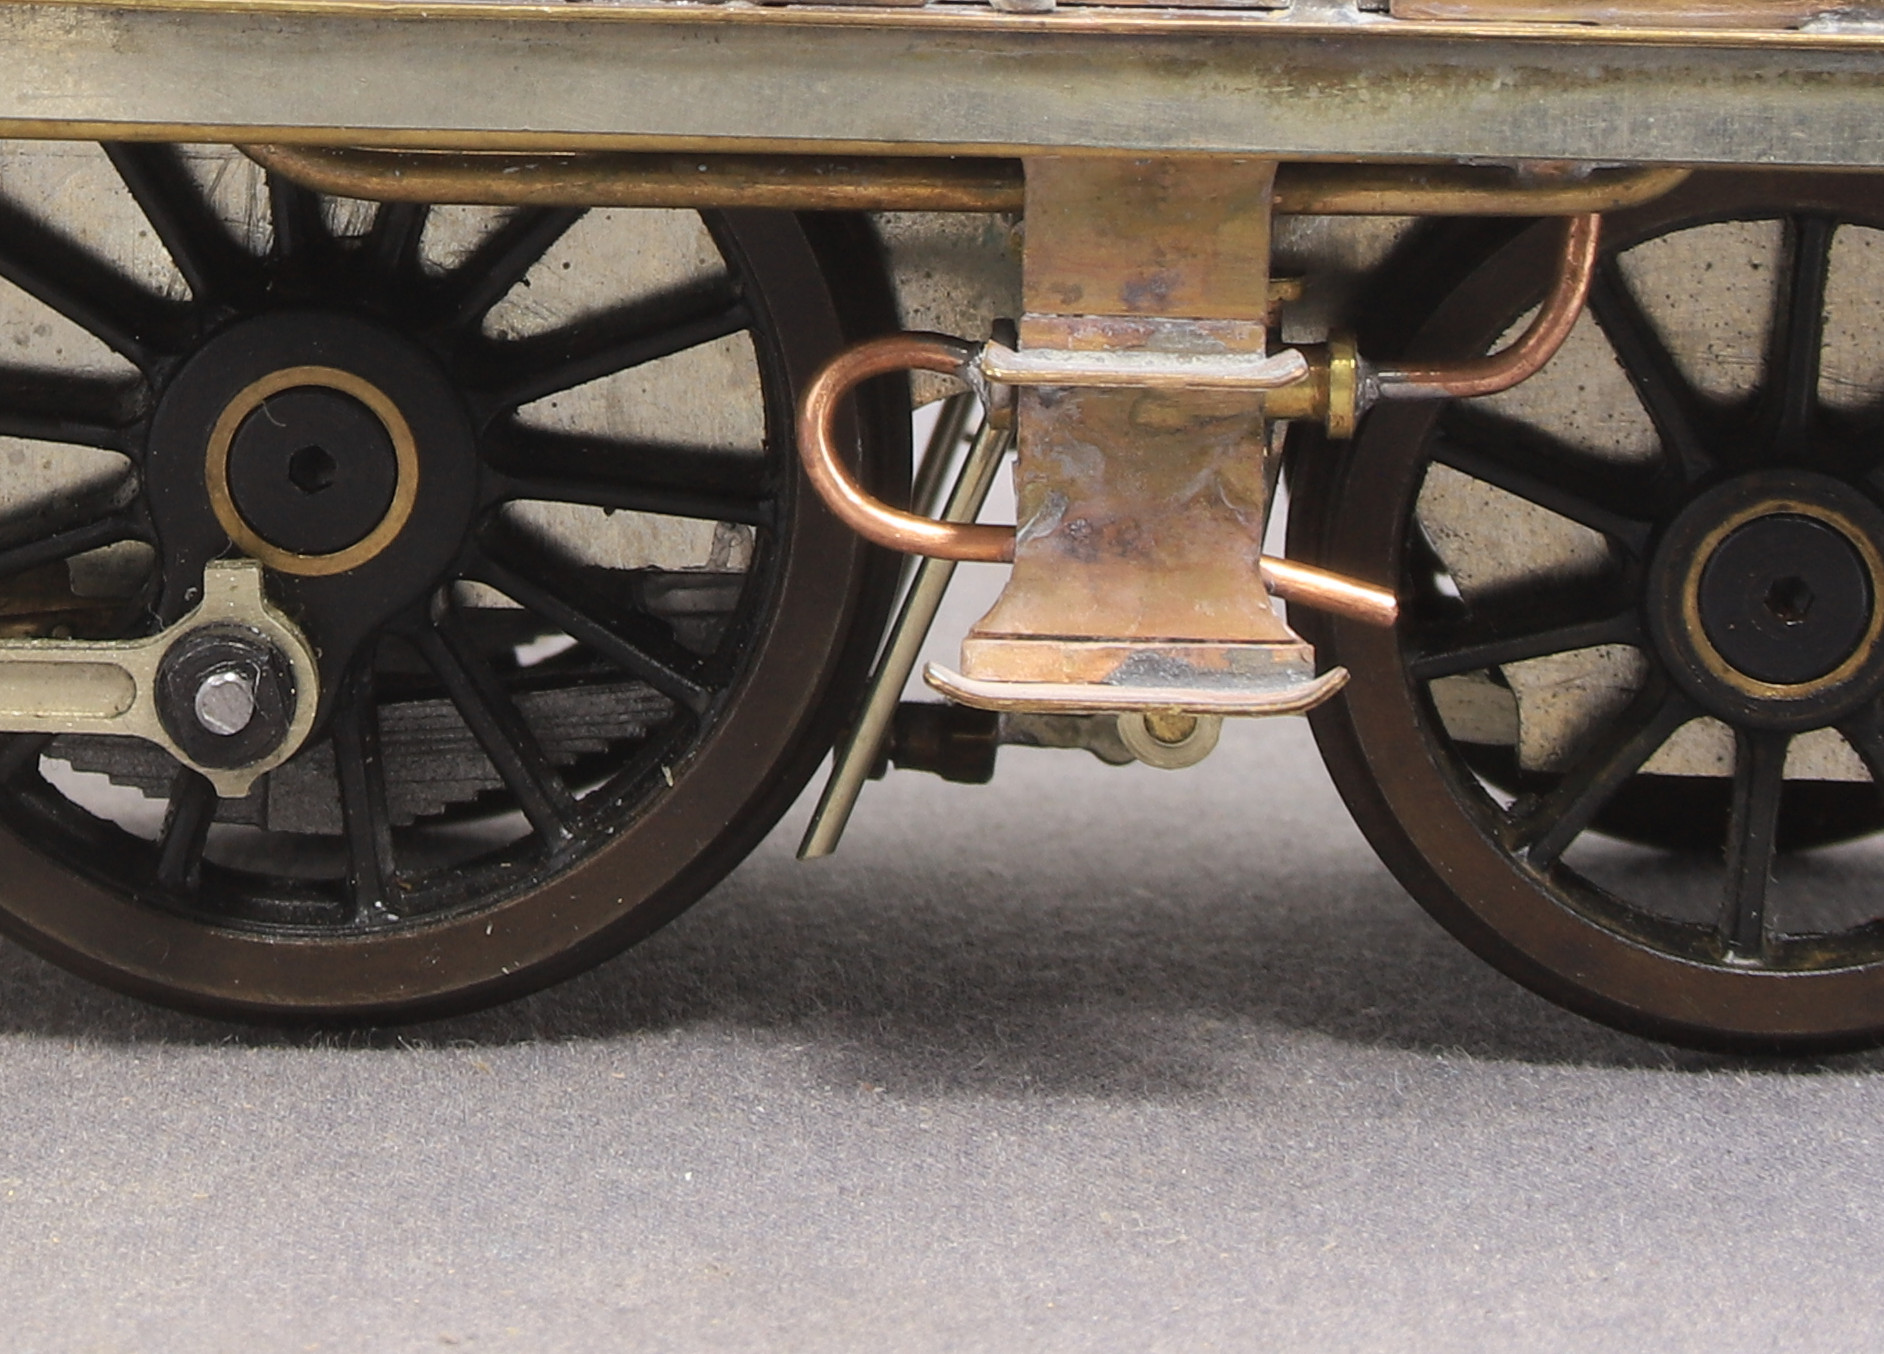
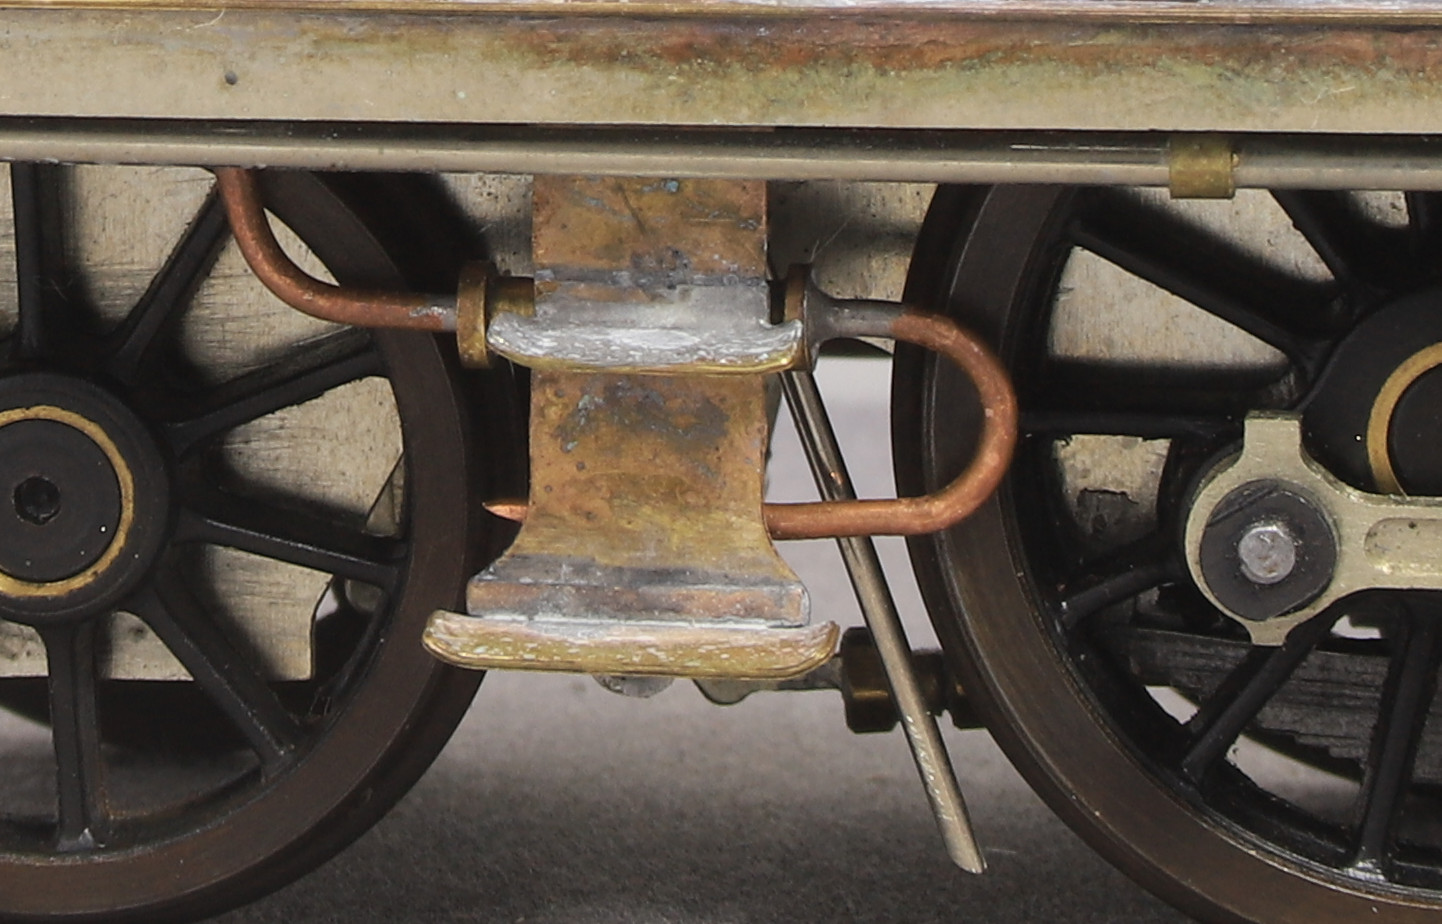
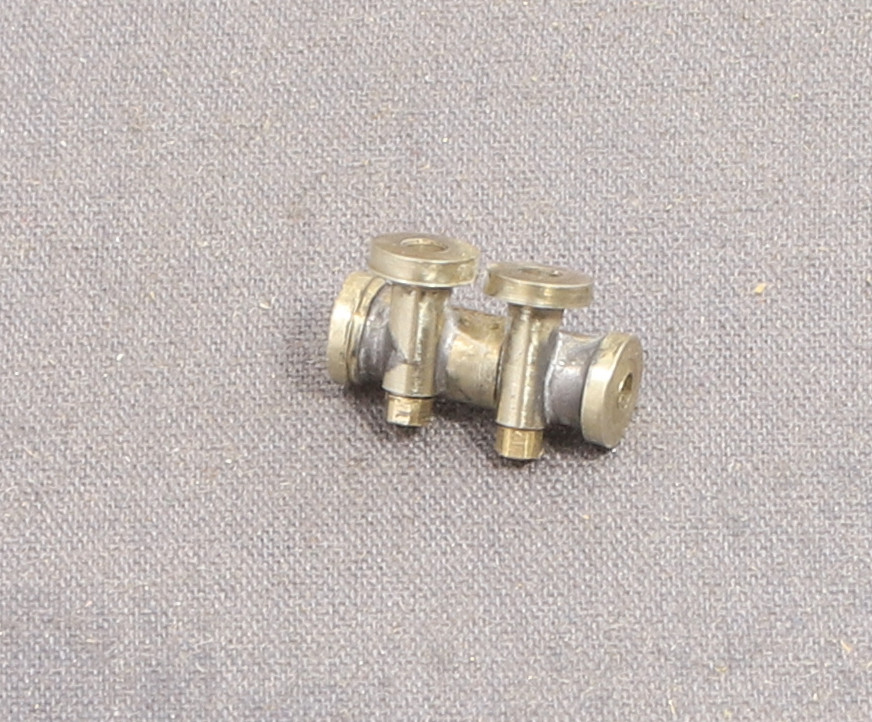
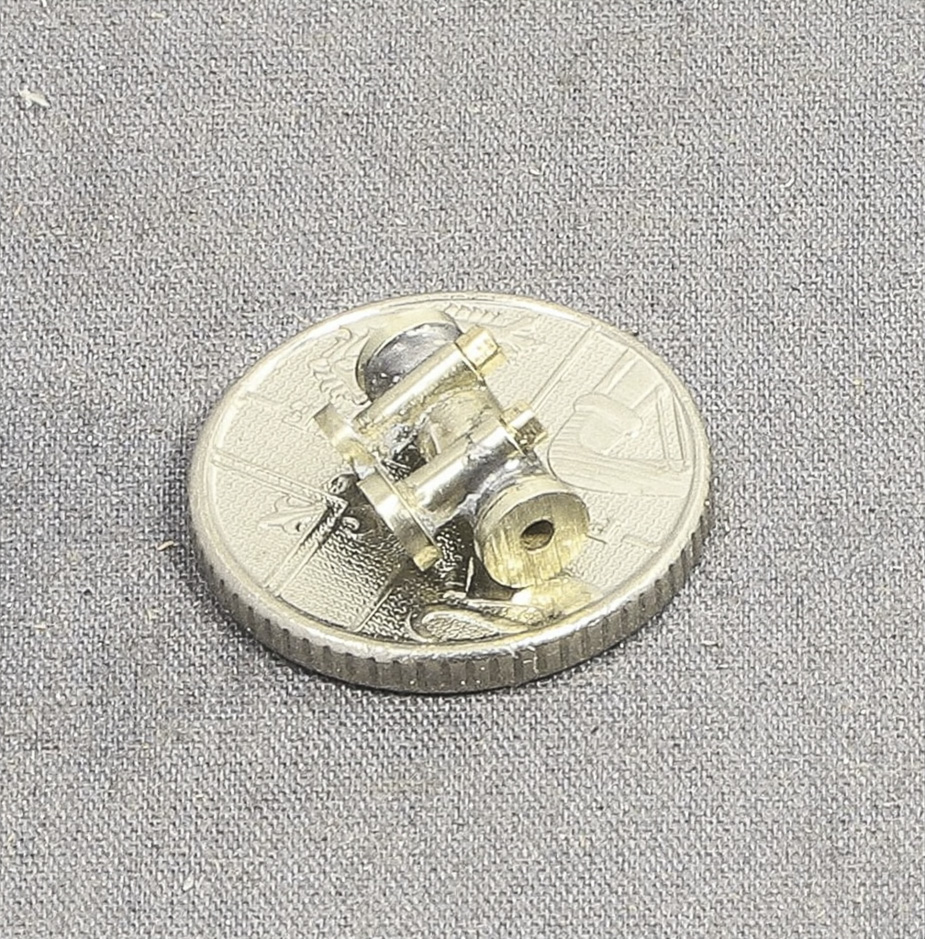
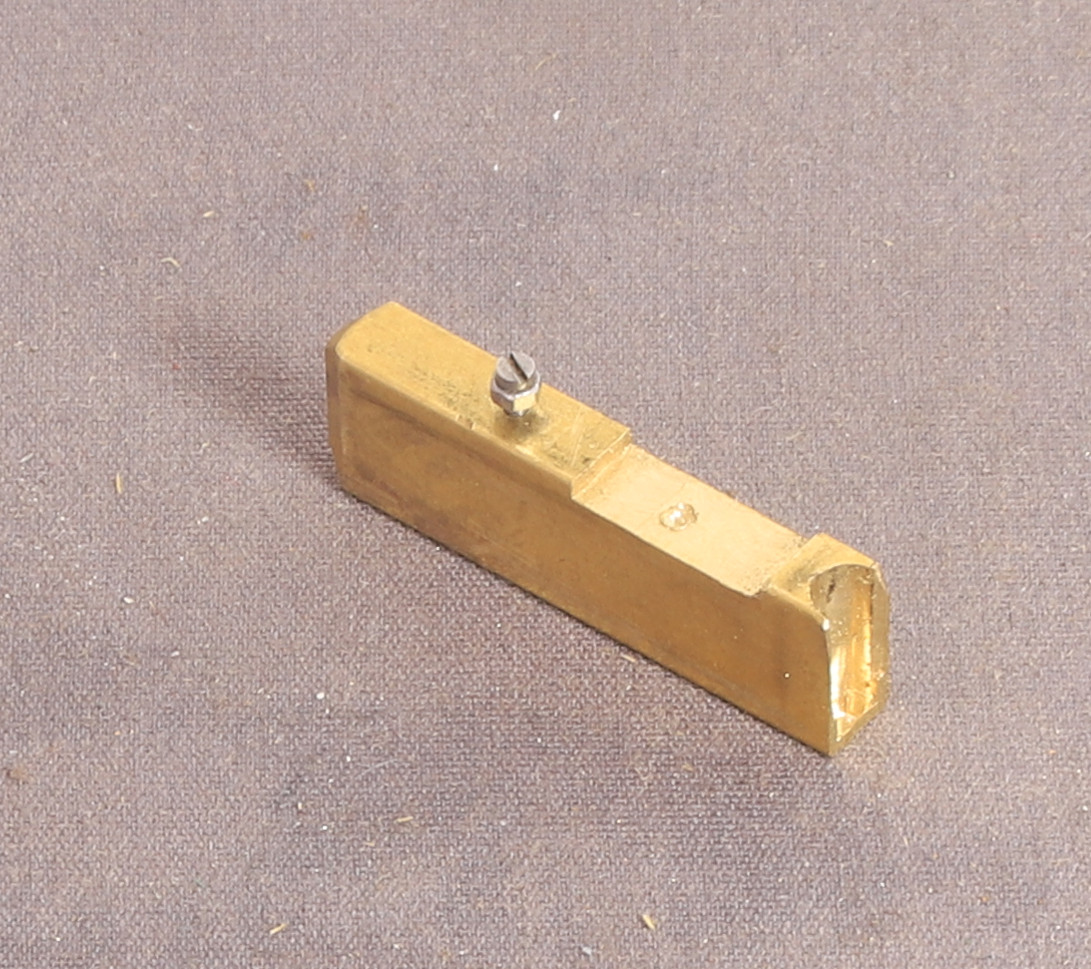
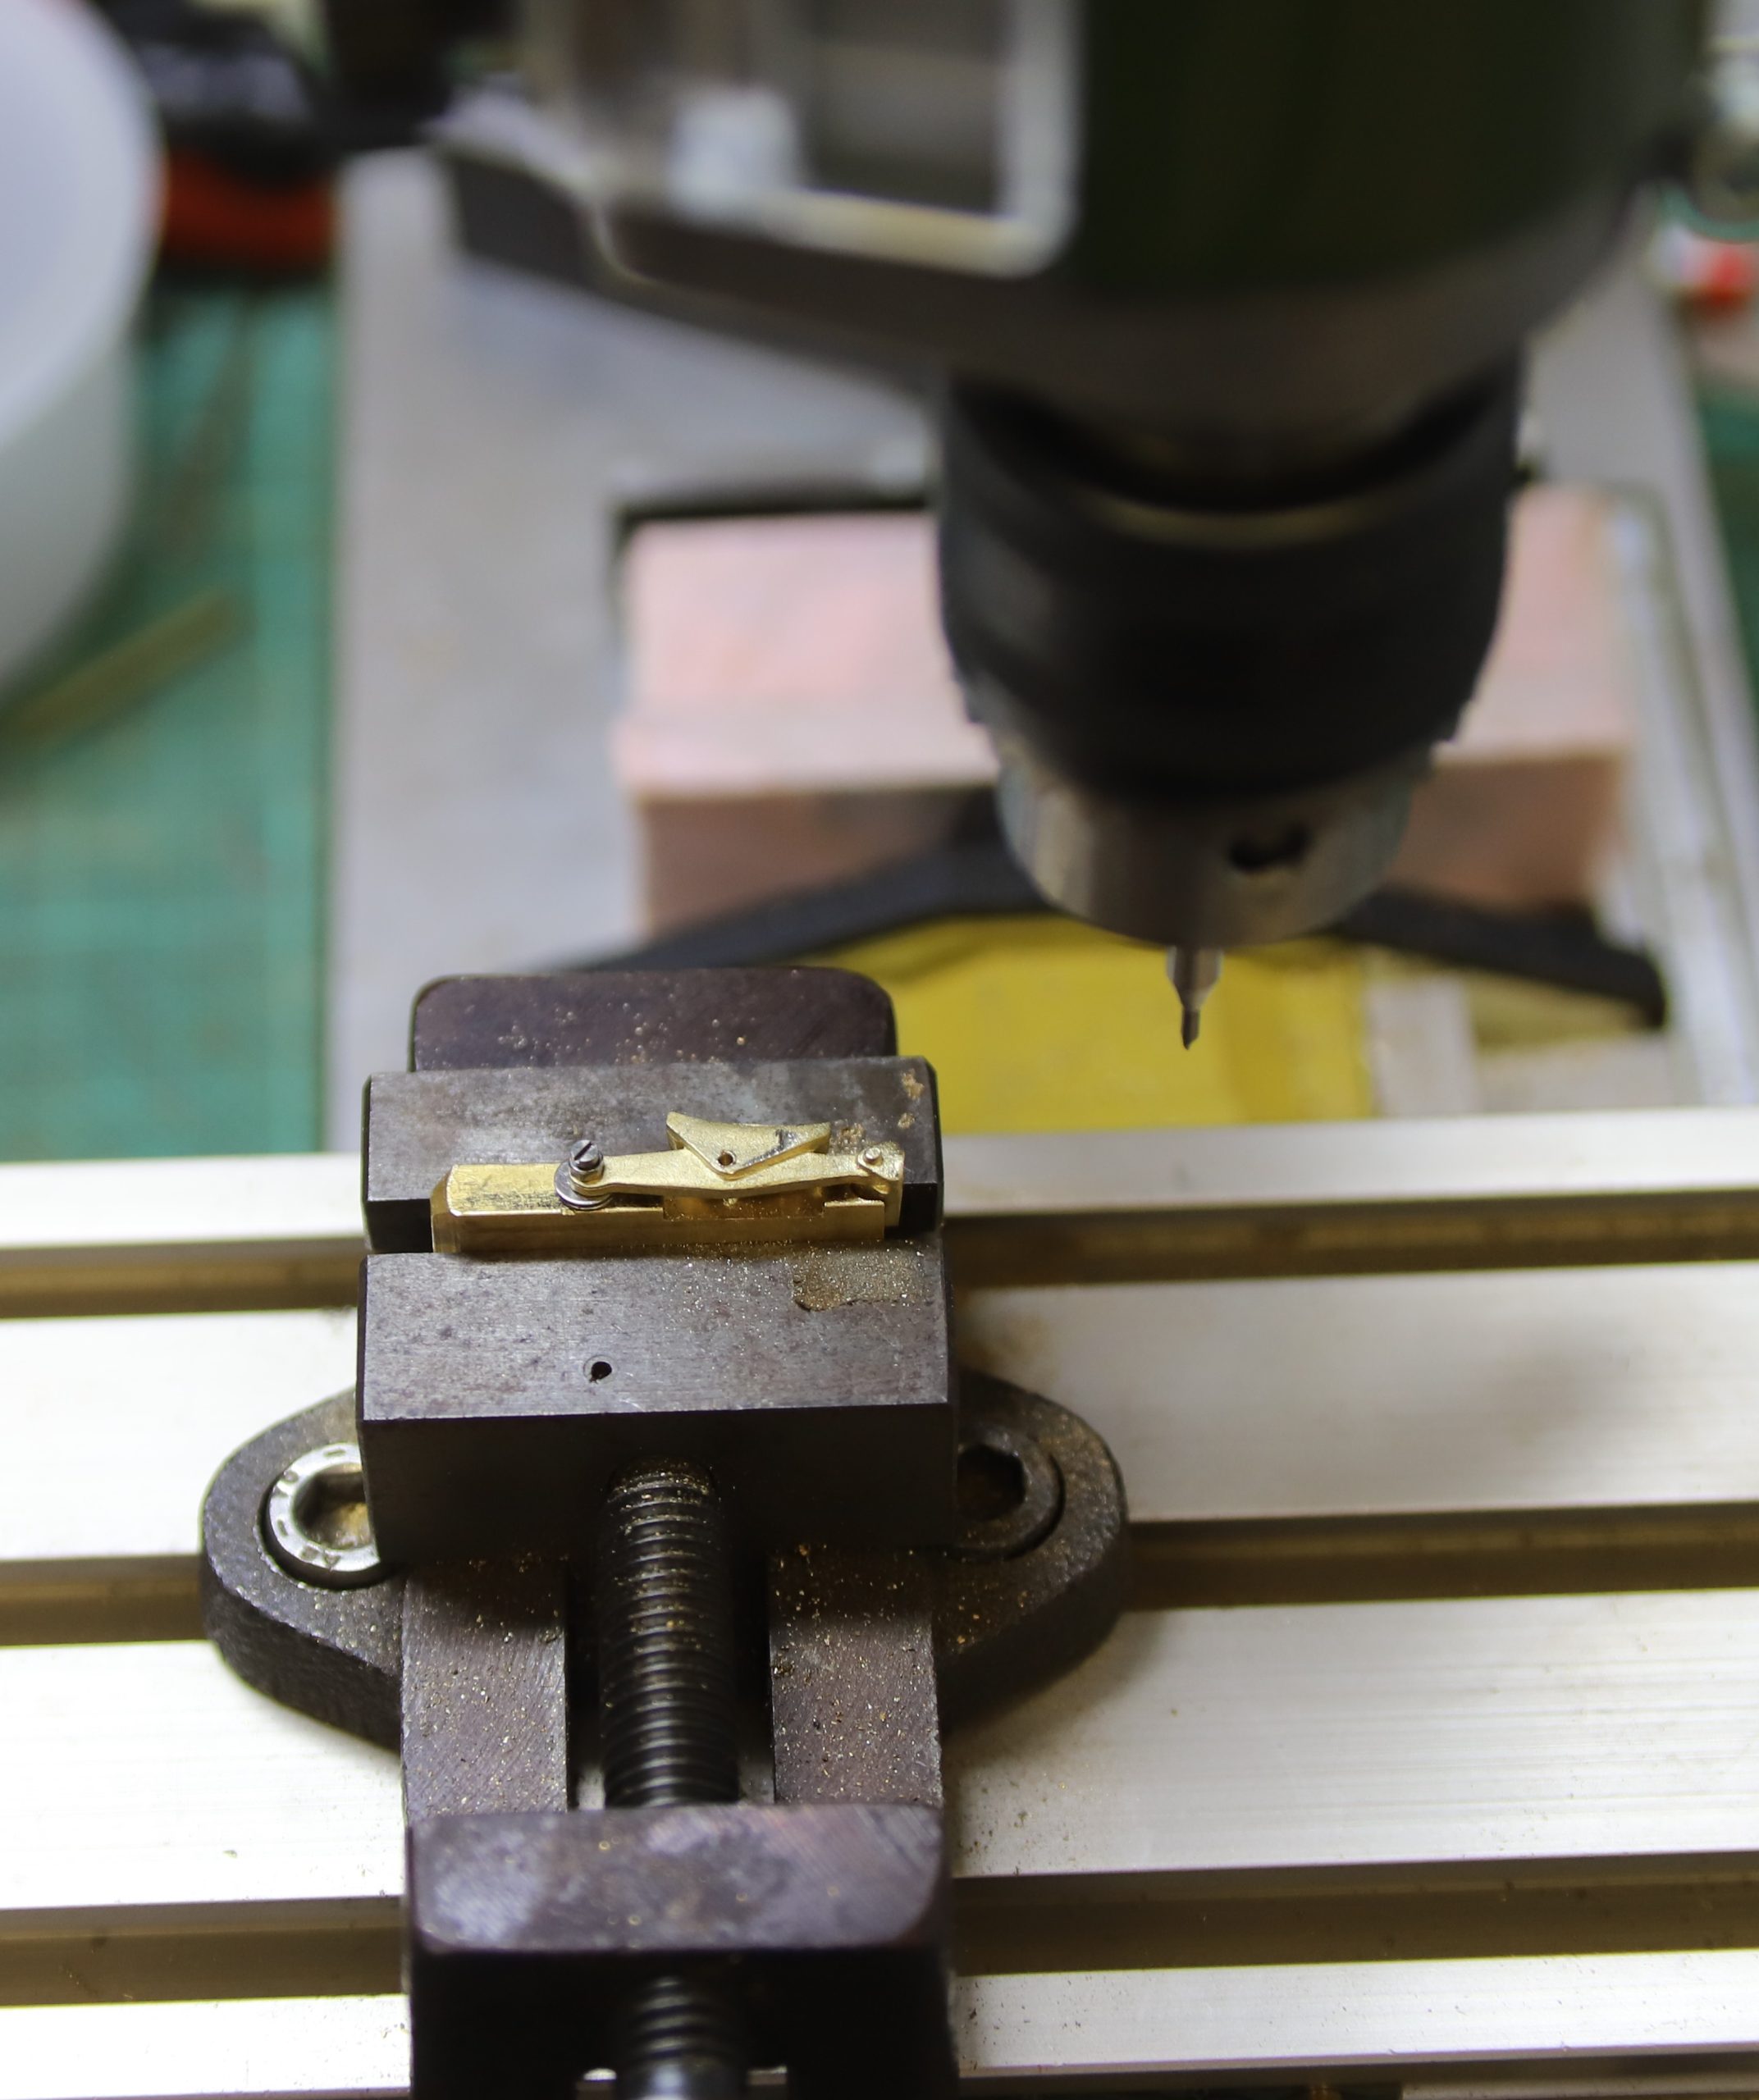
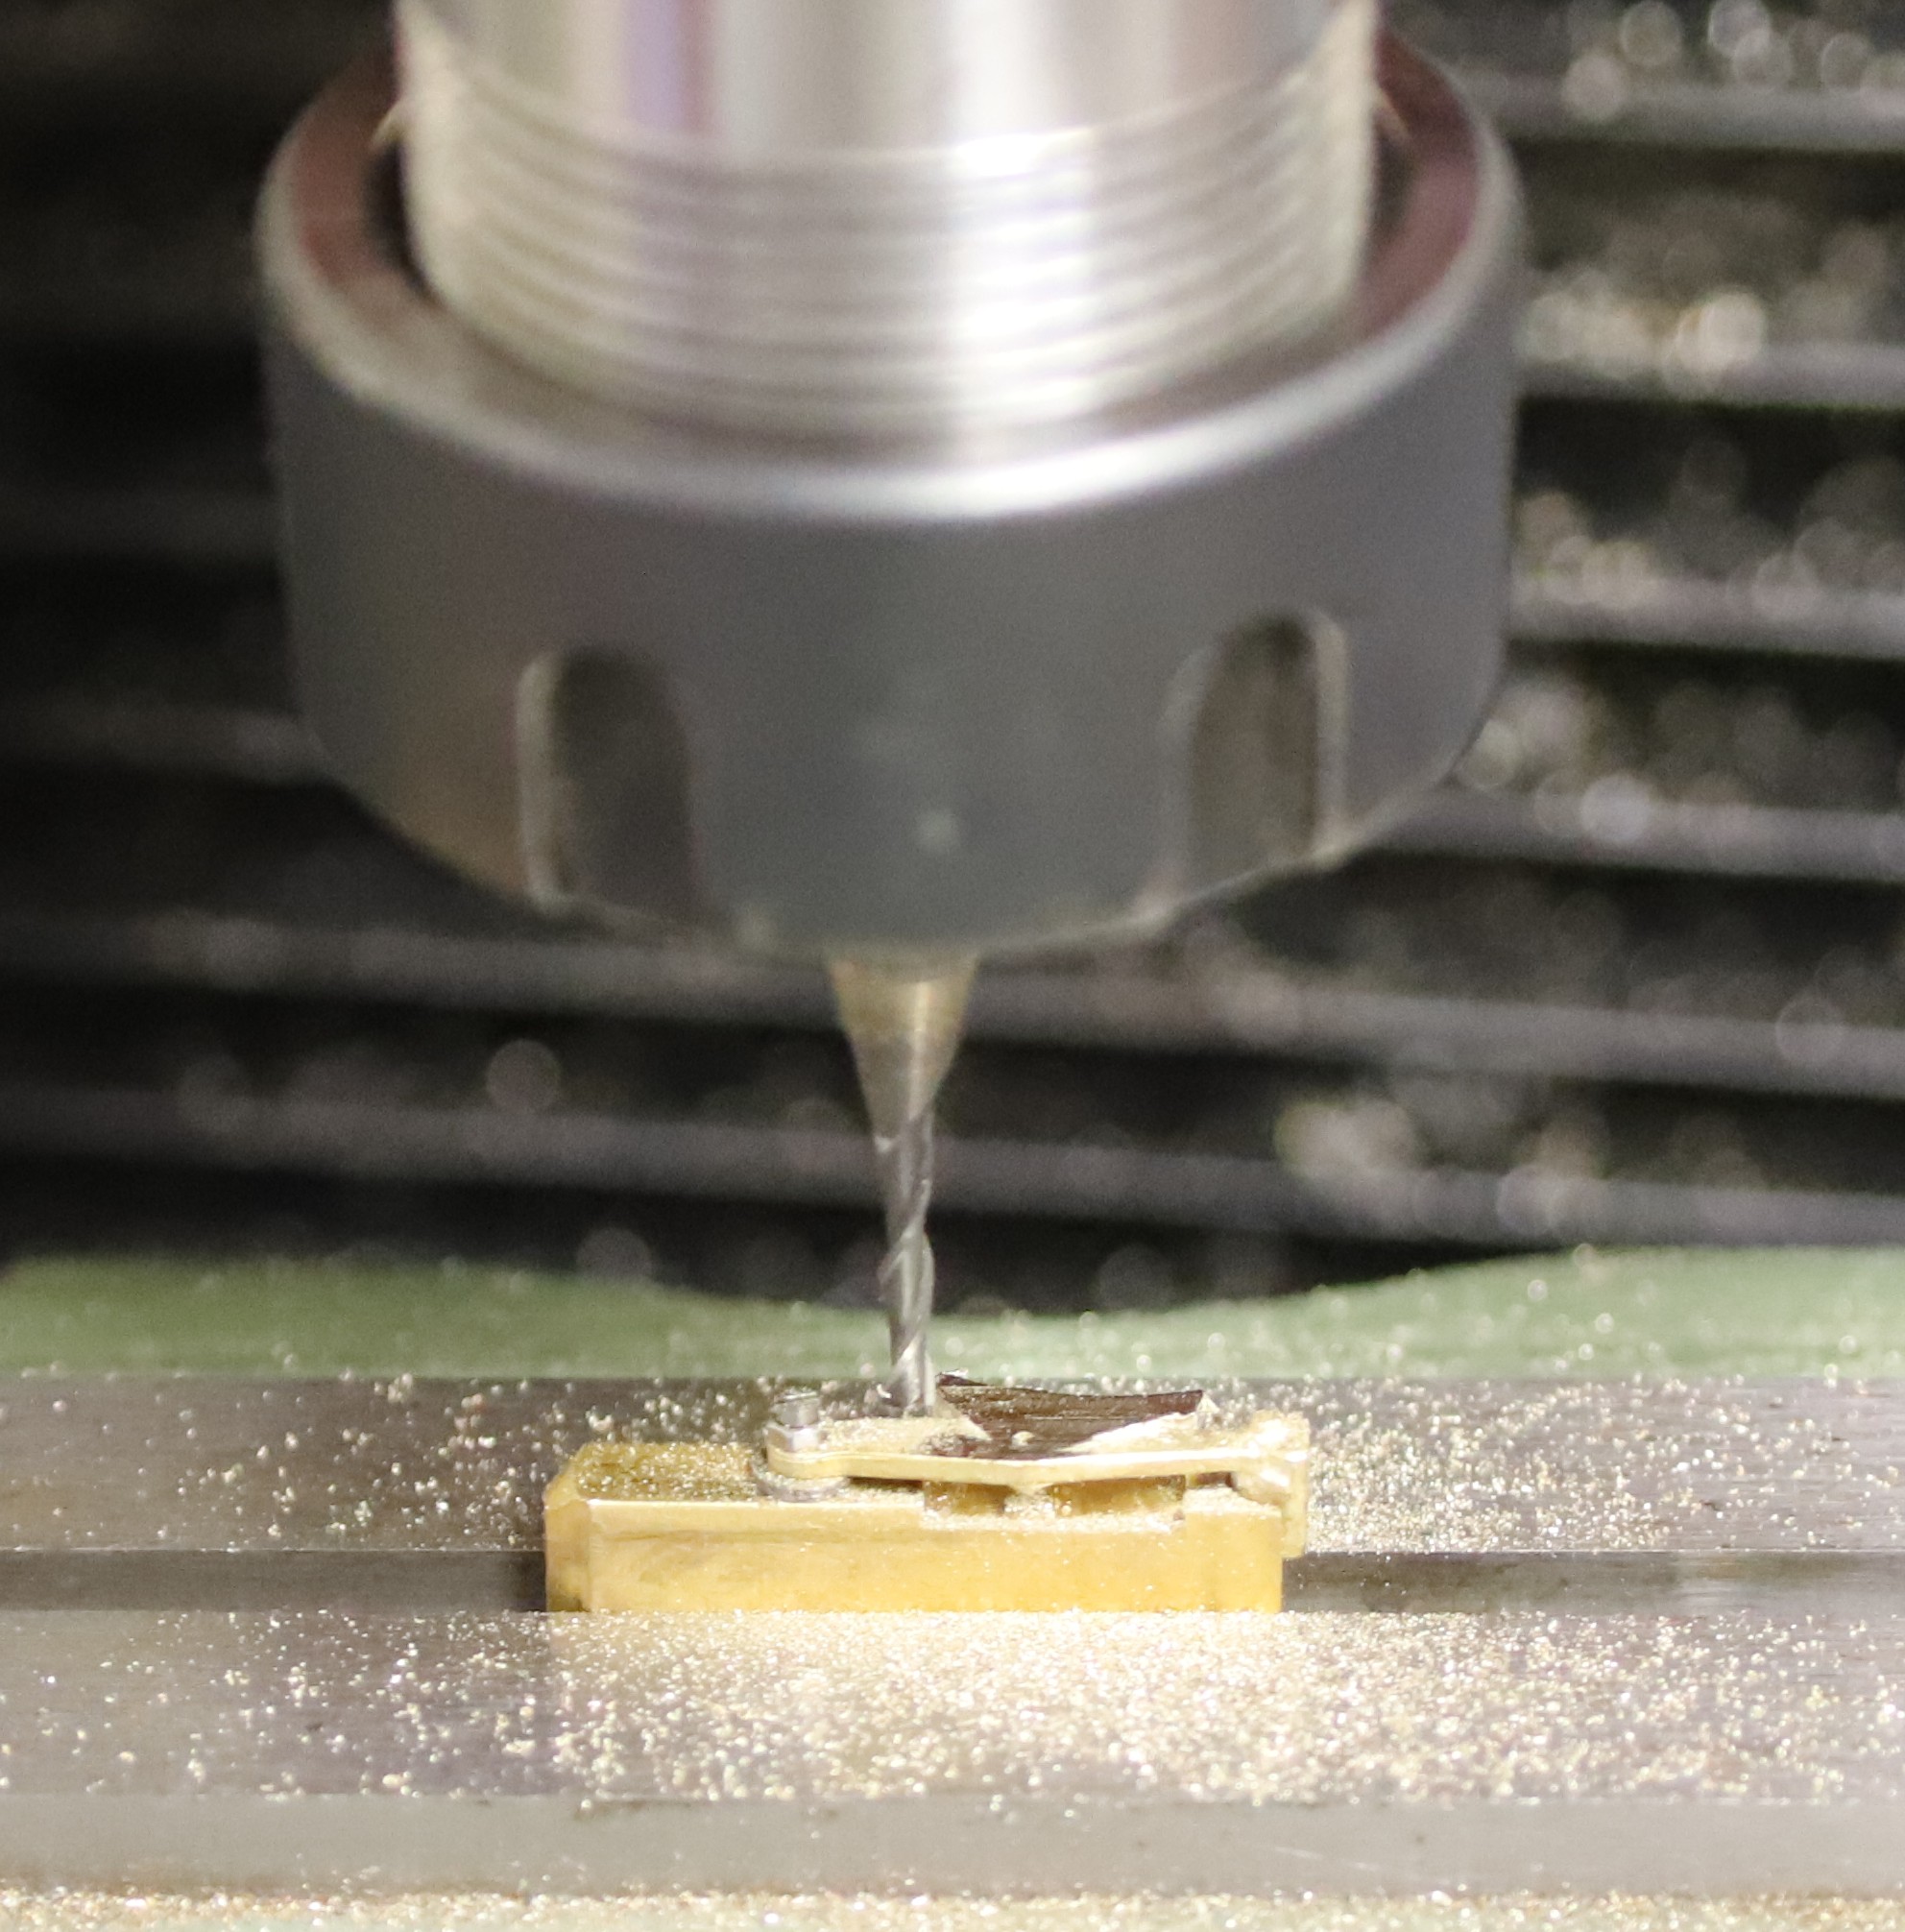
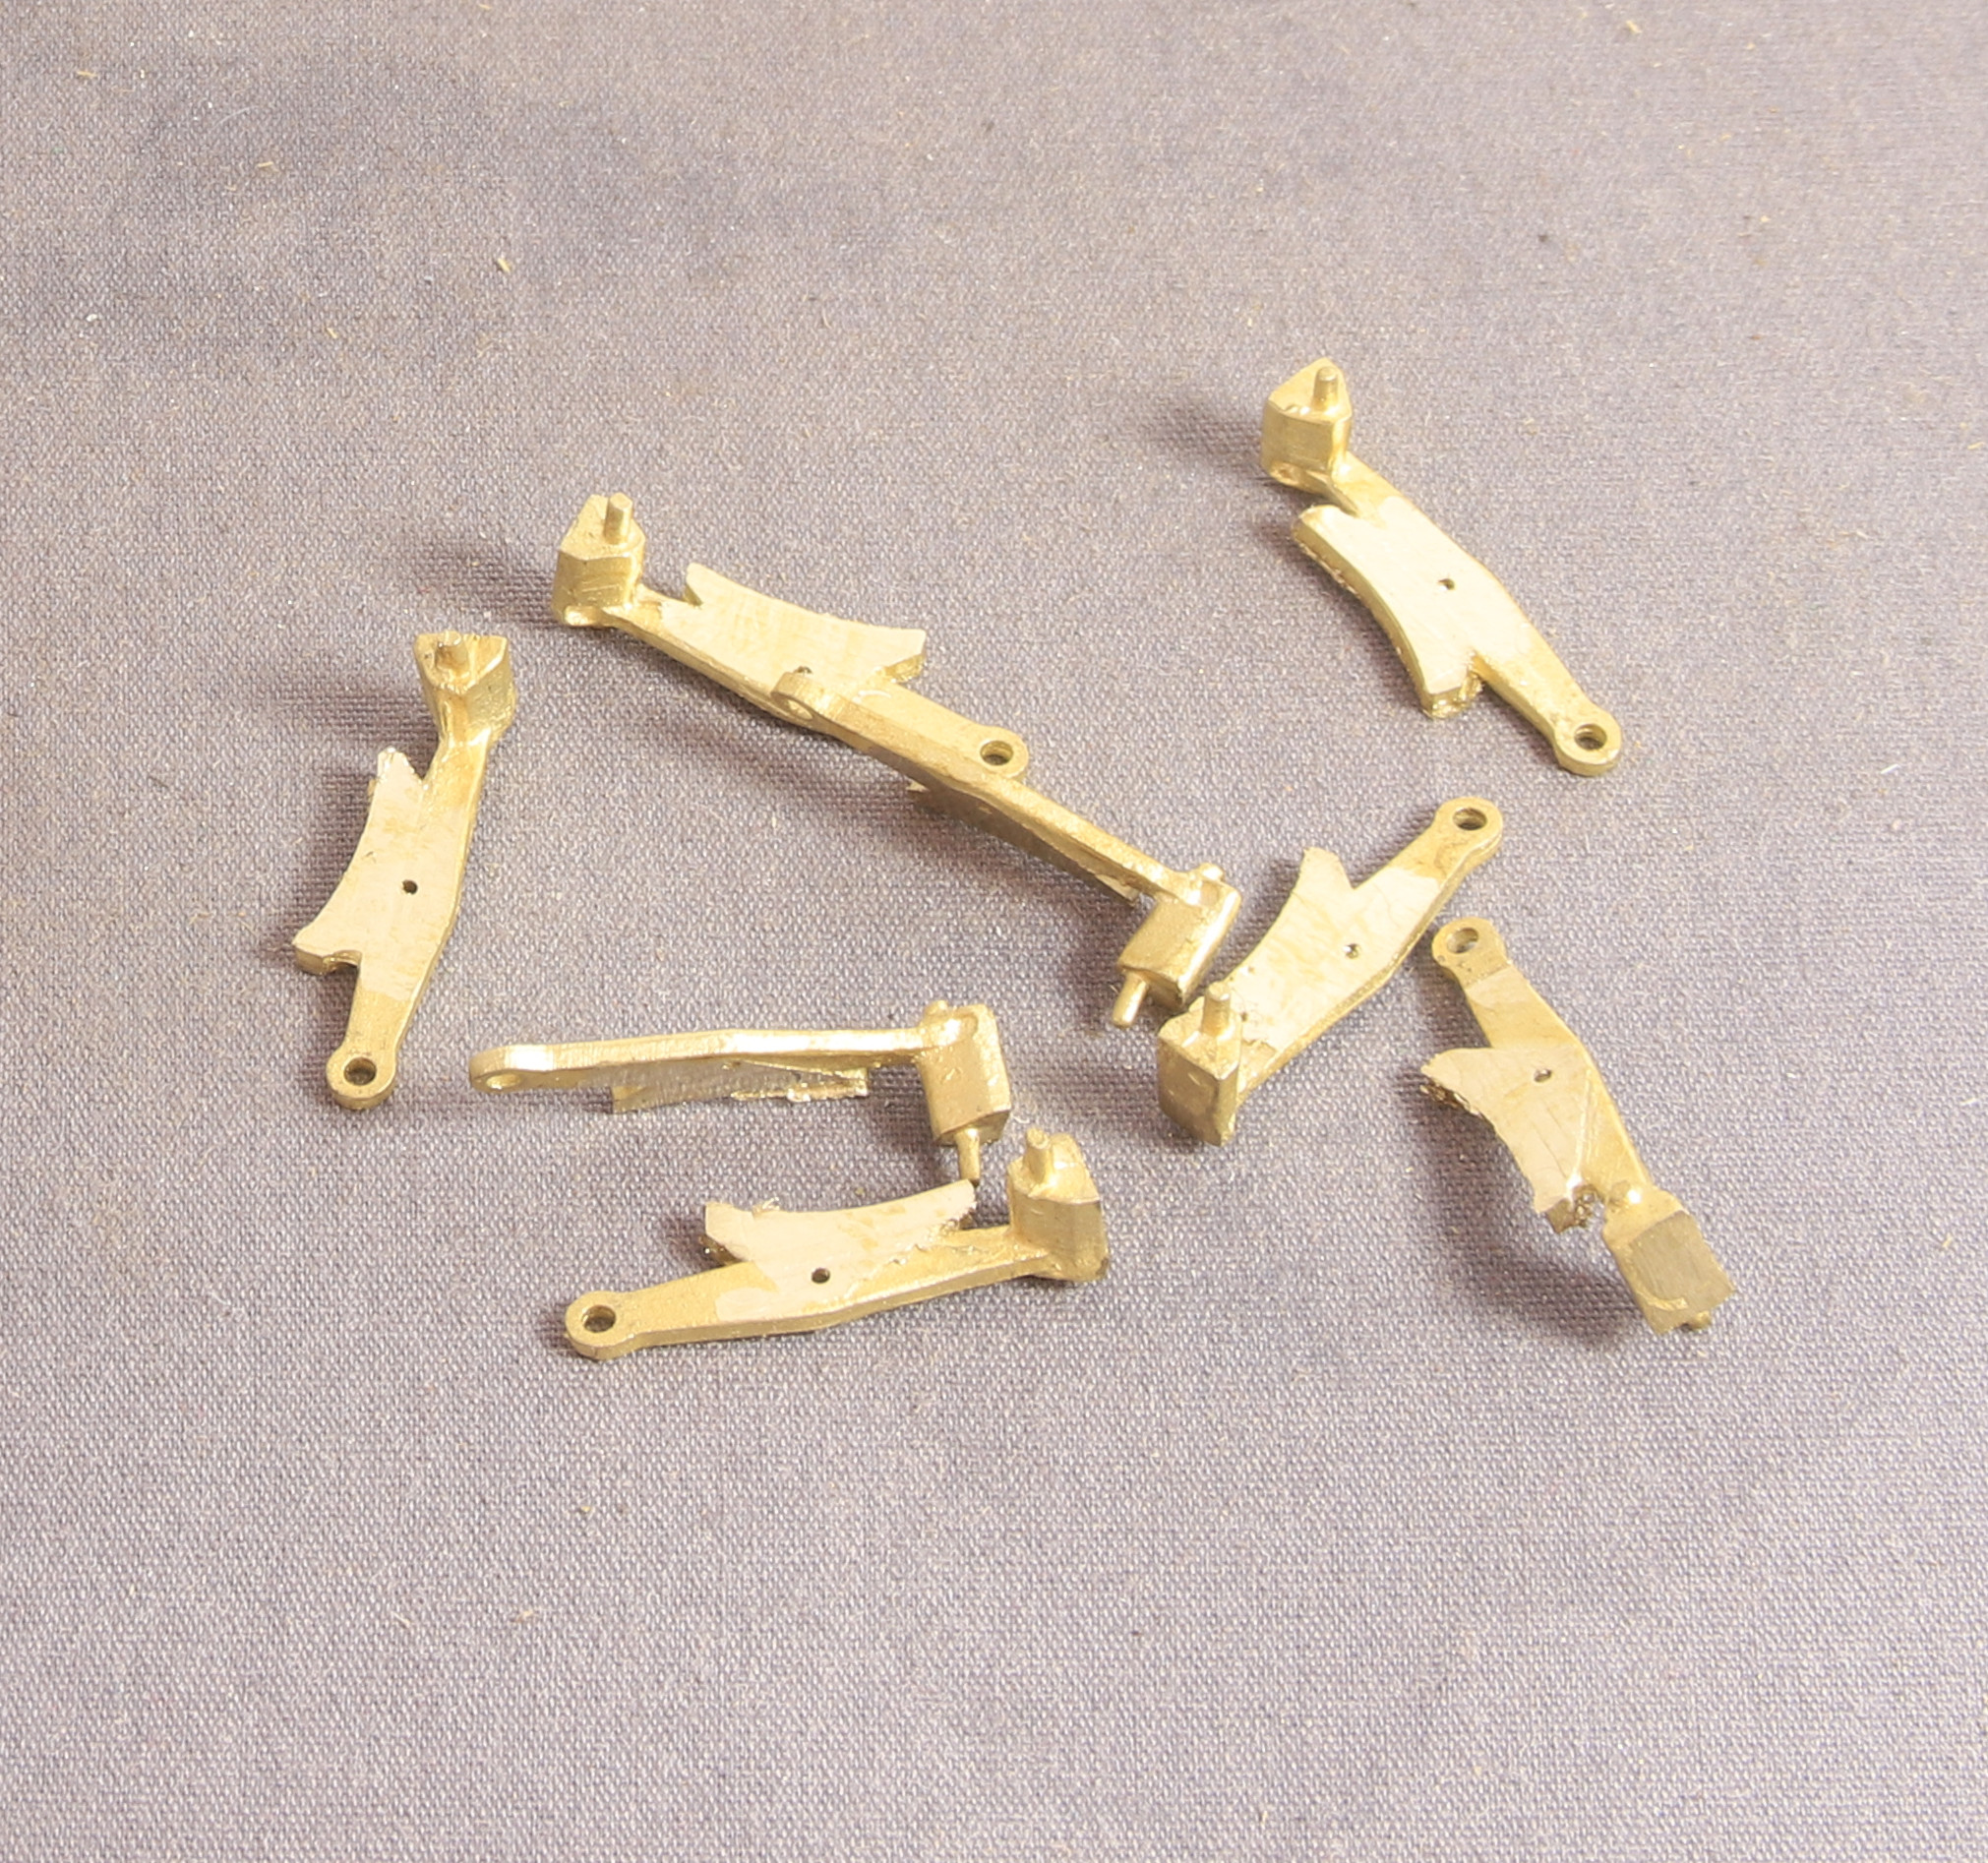
It was only after taking what I thought would be the final construction photos that I realised that I hadn’t added any injectors. To be fair they are easy to miss because they sit behind the cab steps and are very hard to see on photos. not having any real idea what they actually look like I decided to make up something that looks the part while not strictly speaking being accurate.
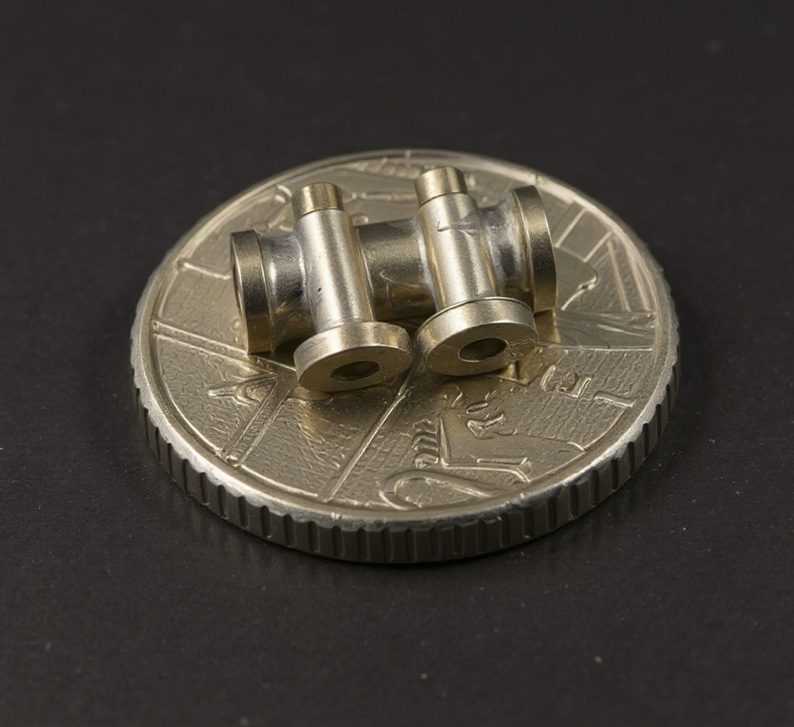
I did a test piece yesterday.
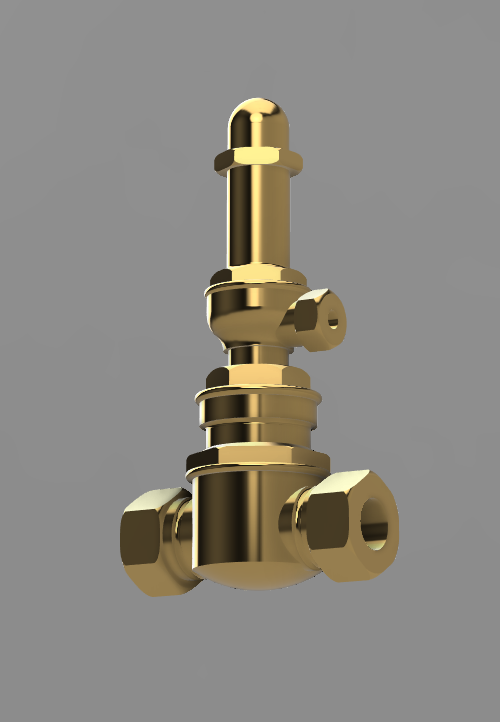
Then I ran it through the Ai function of Adobe Express photos again and this is what it produced – very smart but it’s rounded the hex nuts off.
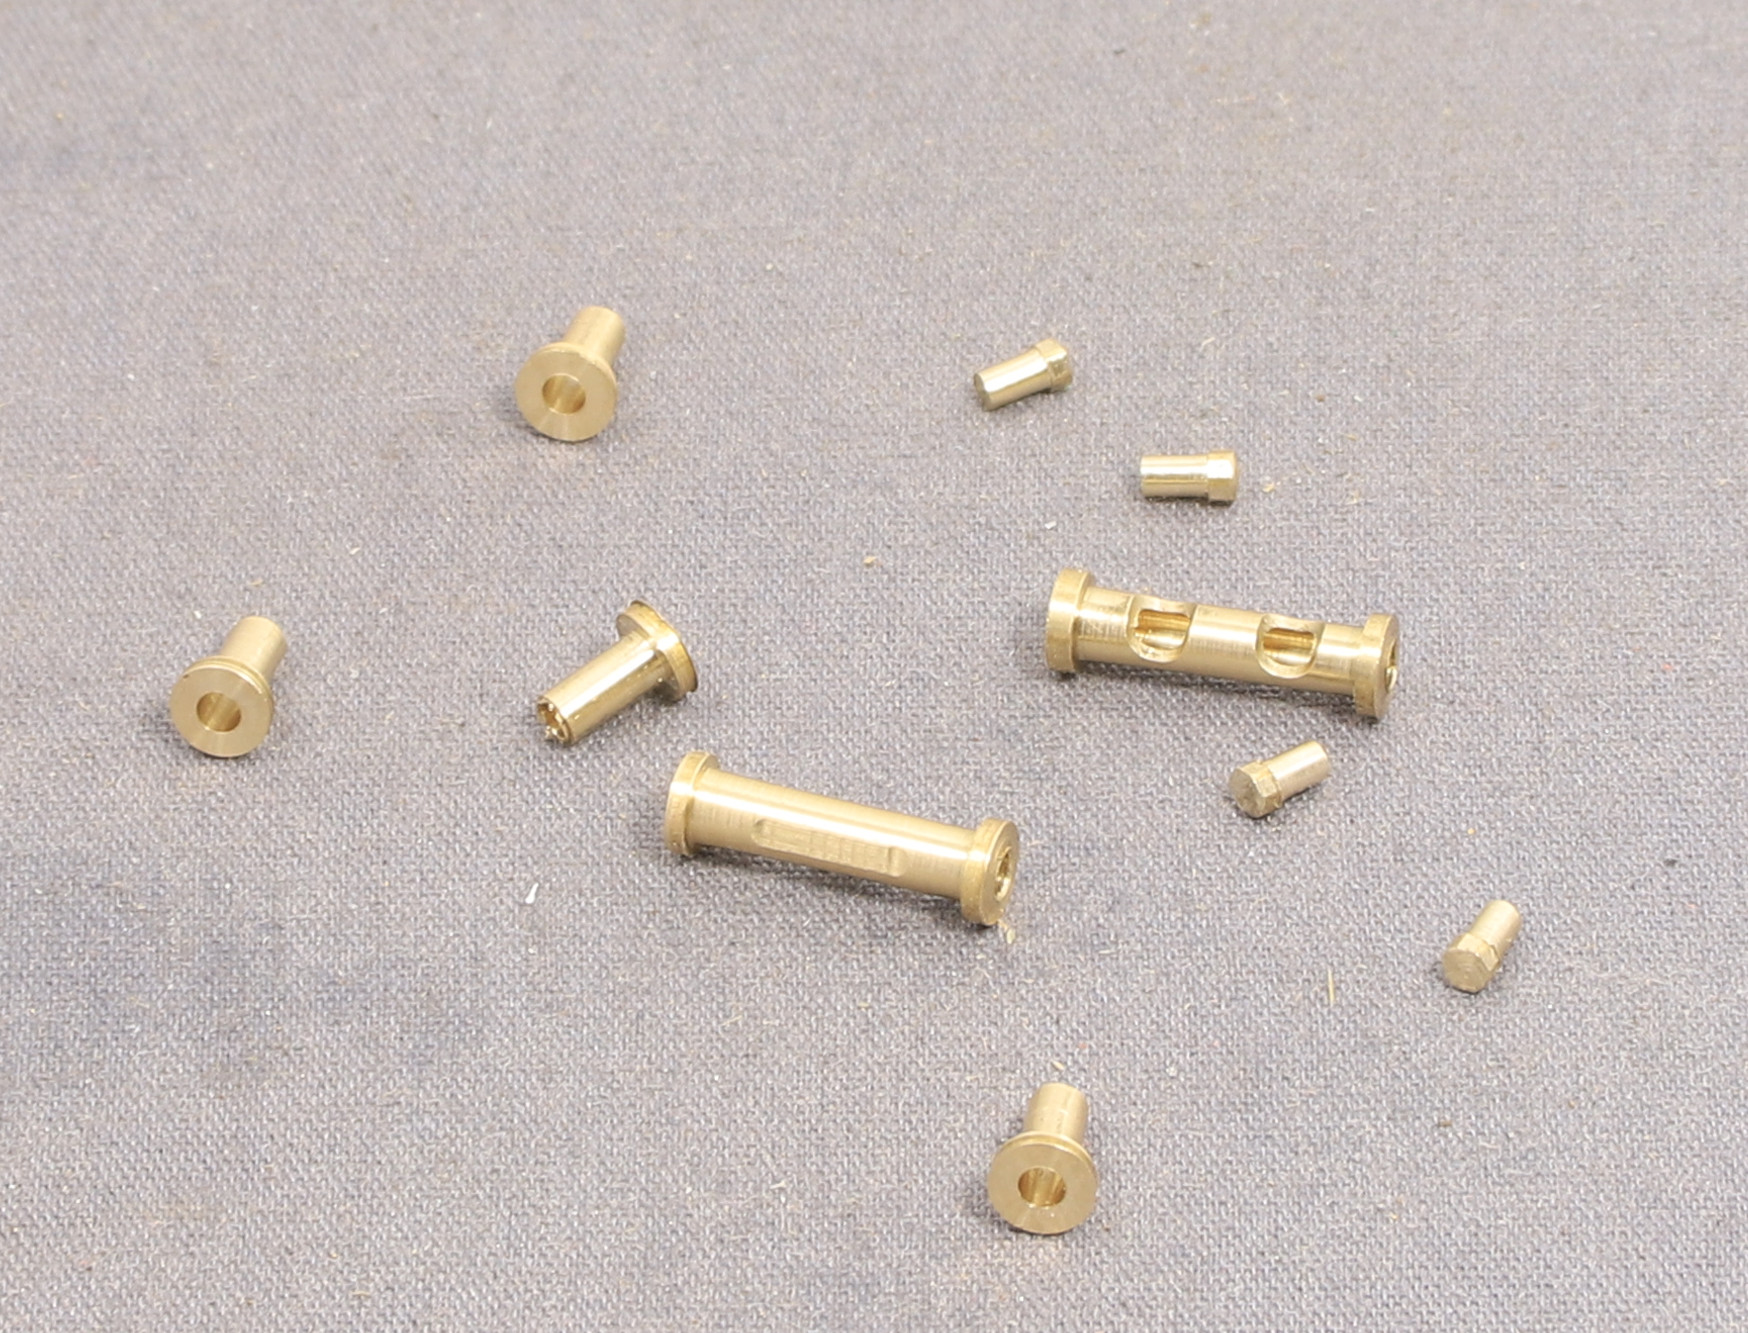
Having done the test piece I realised that everything about it was just a little too big so today I made a pair of smaller ones.
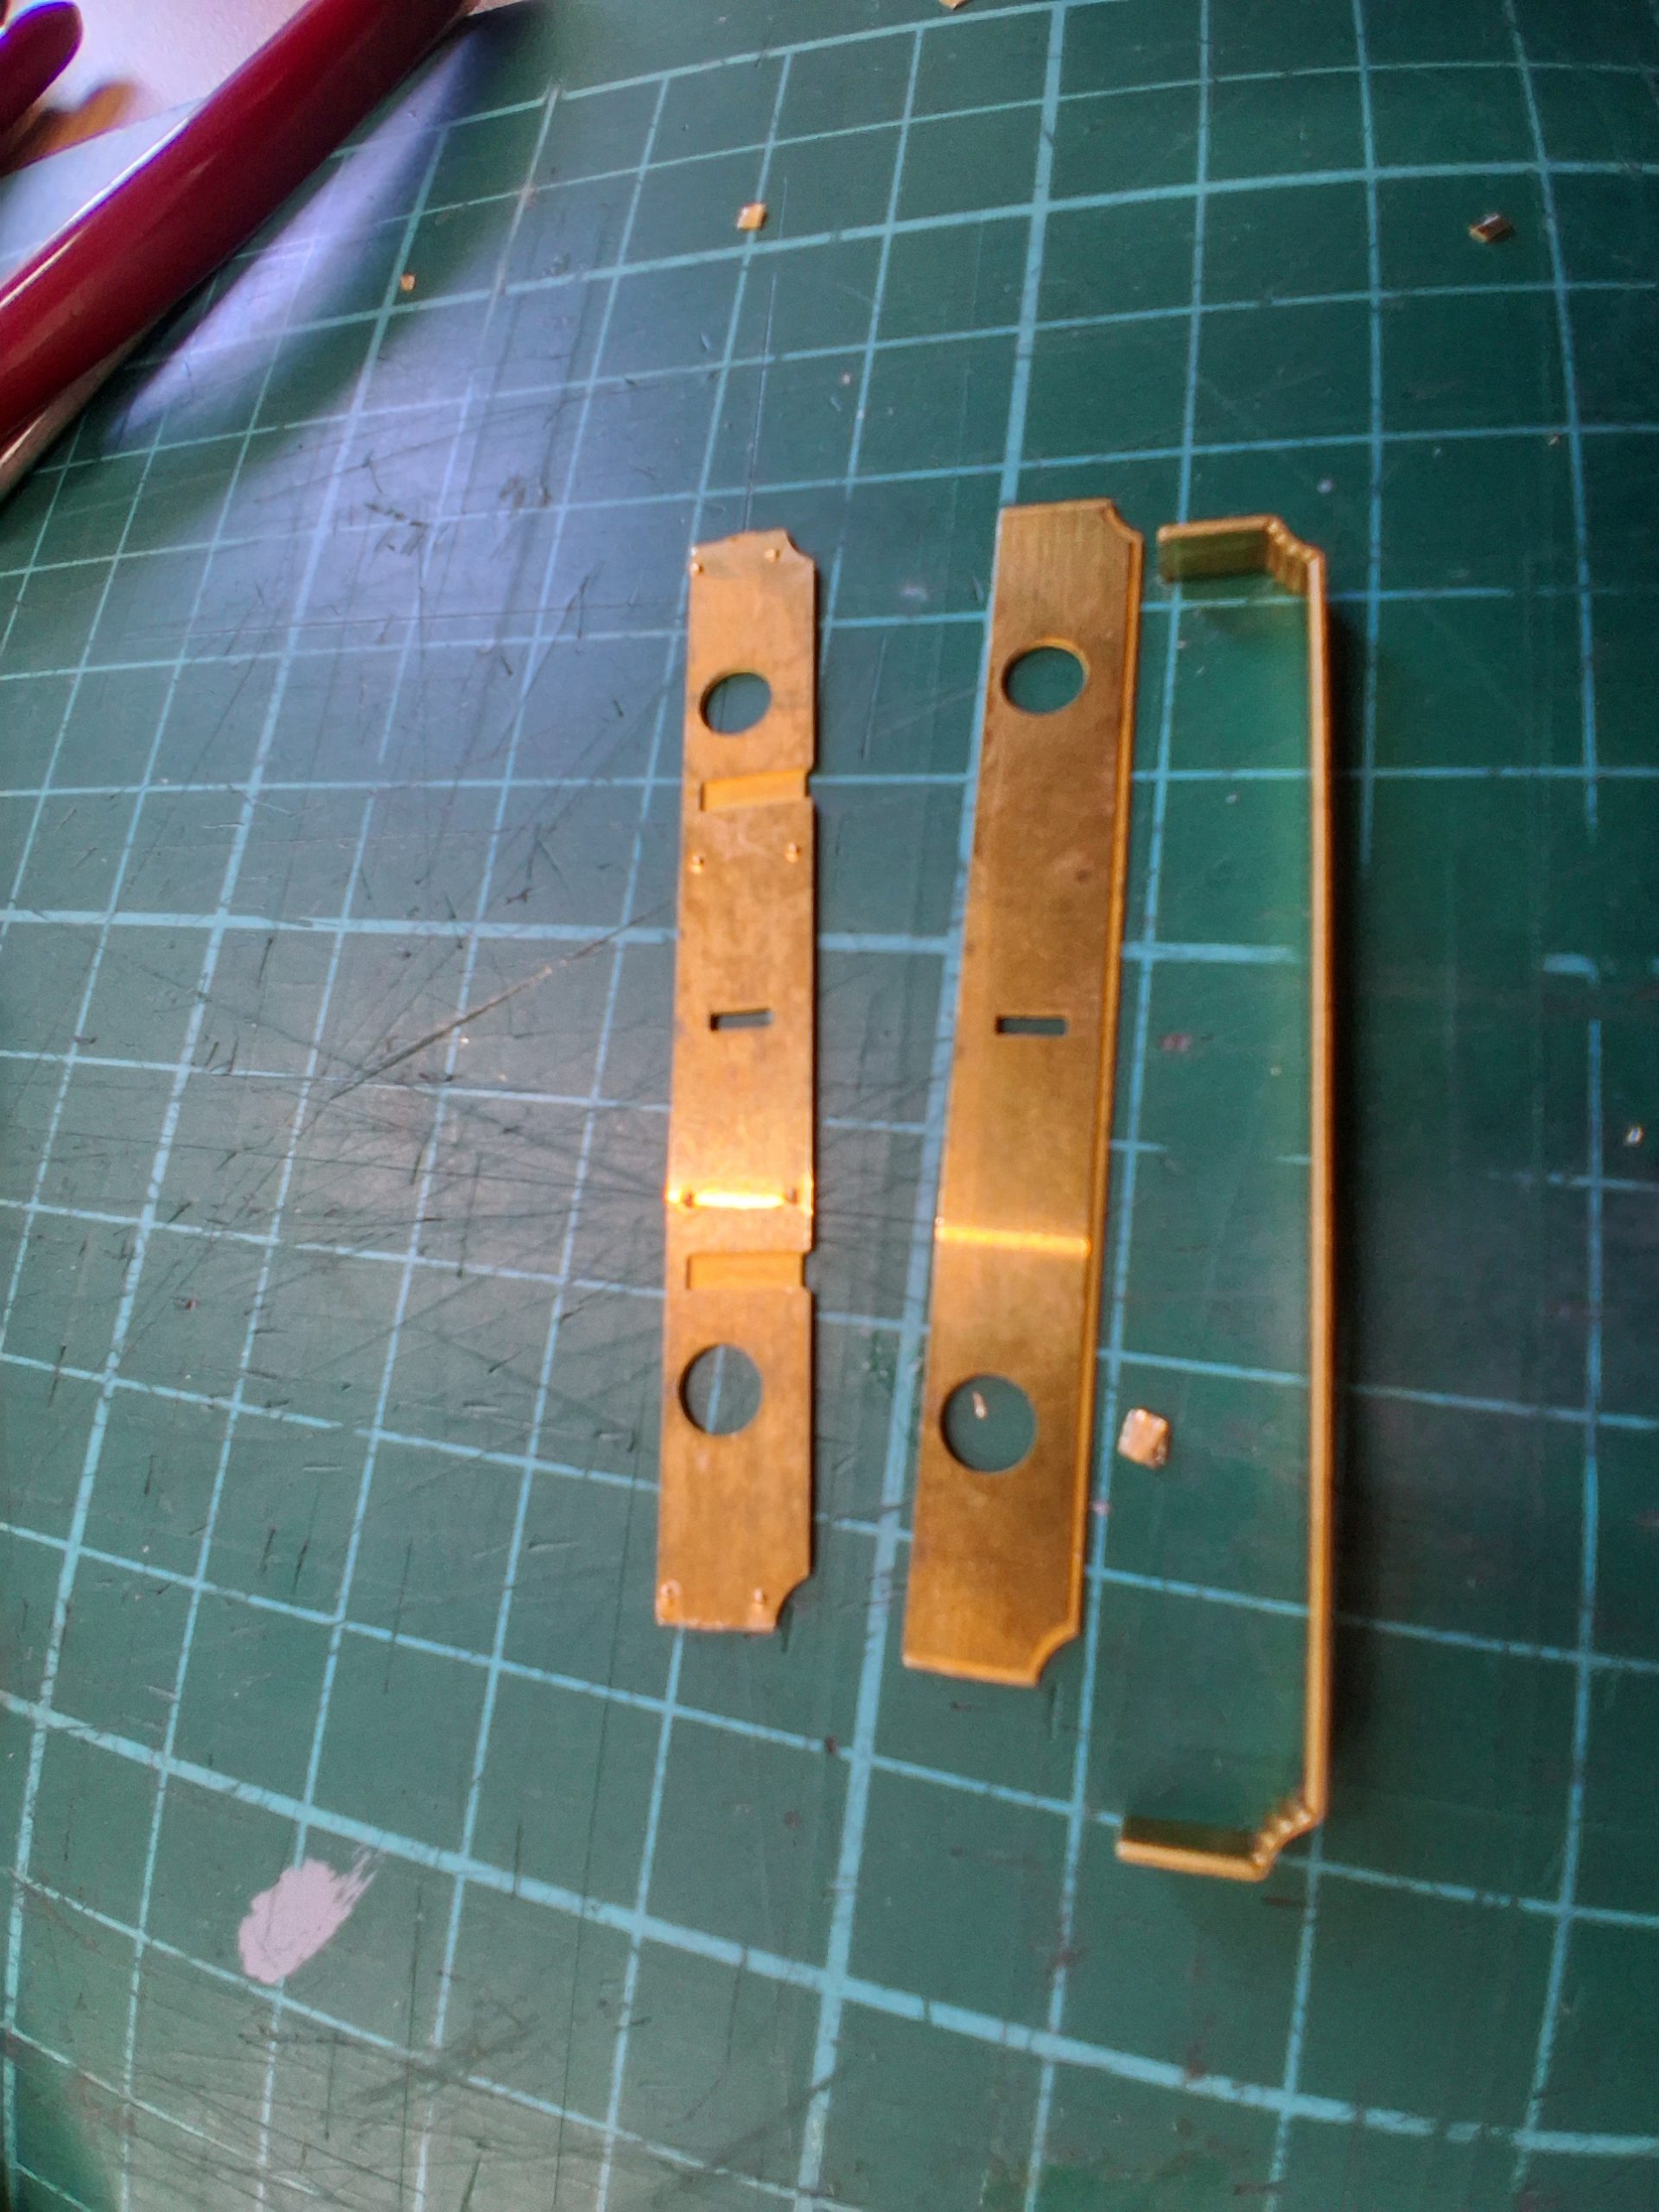
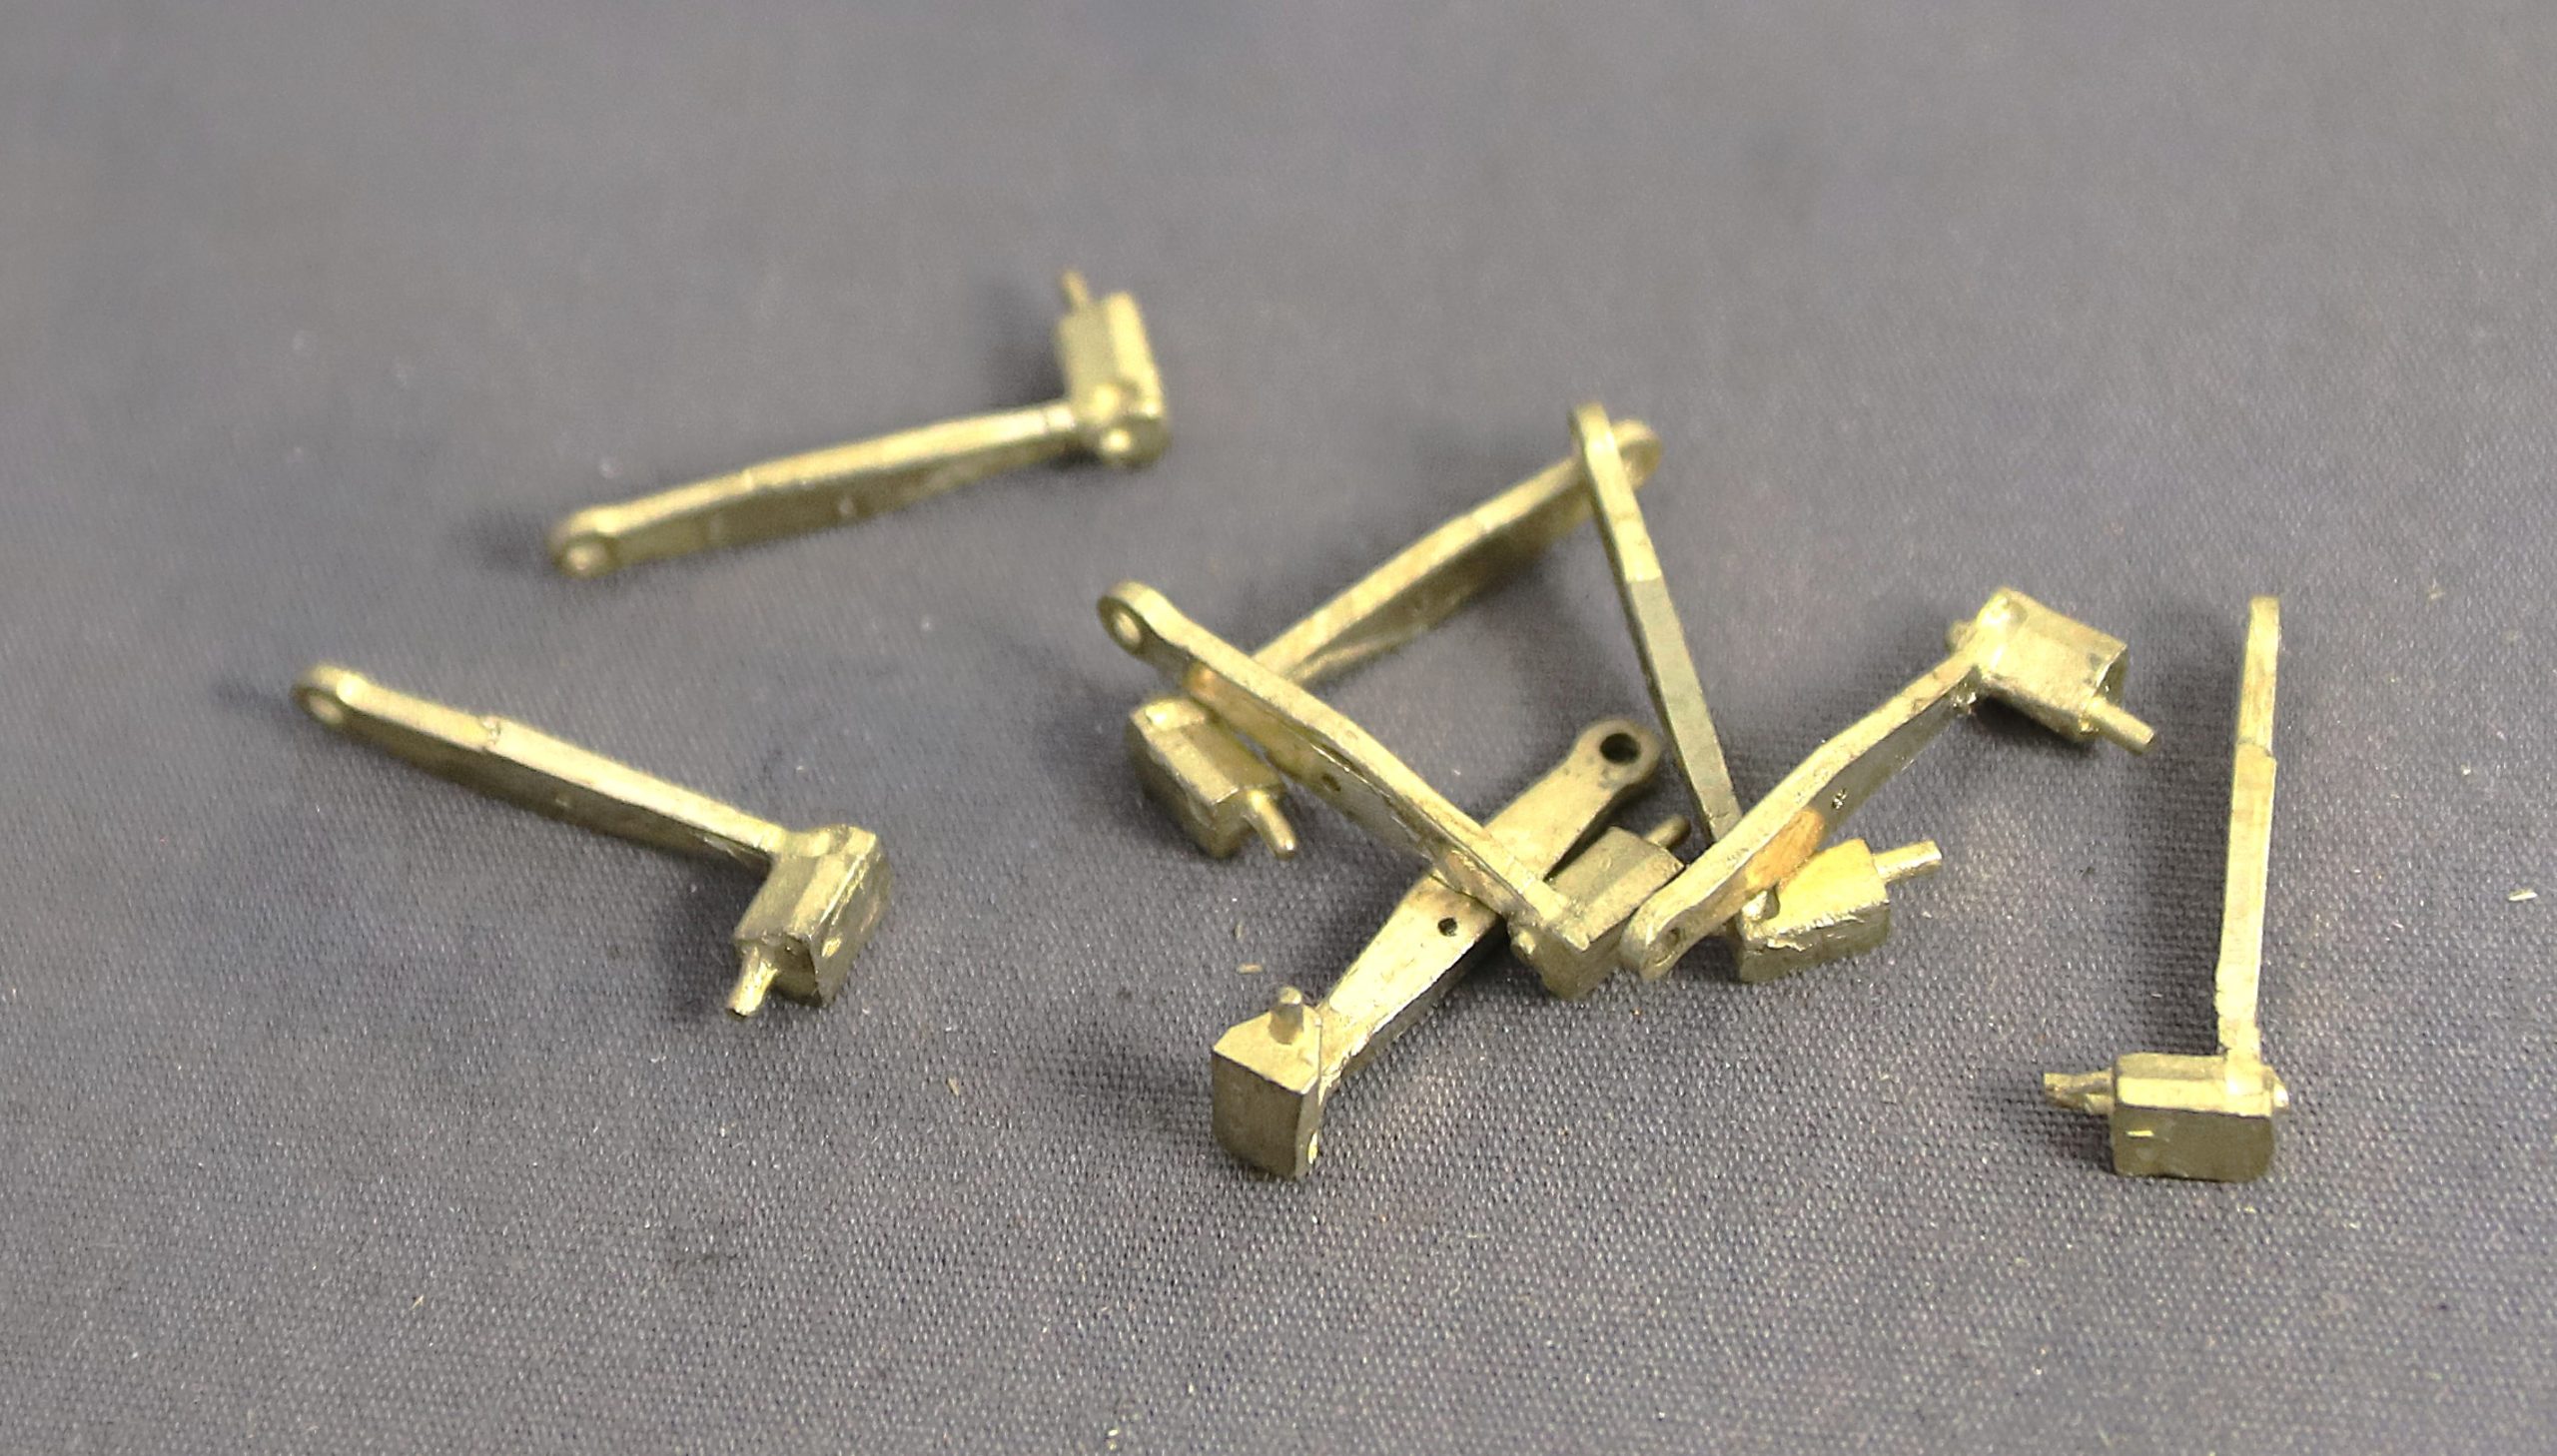
This was the individual parts for them.
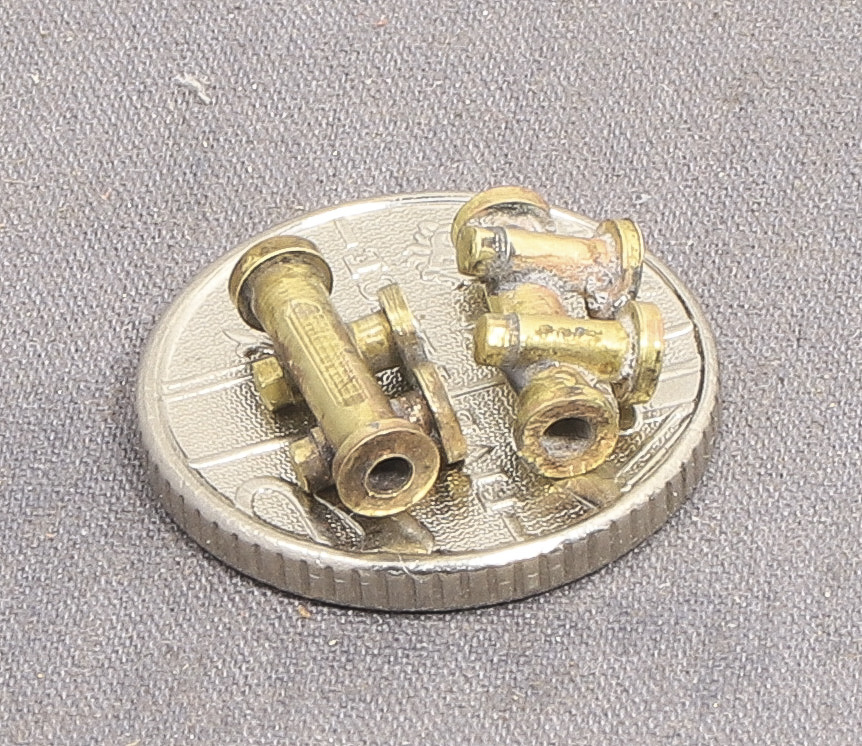
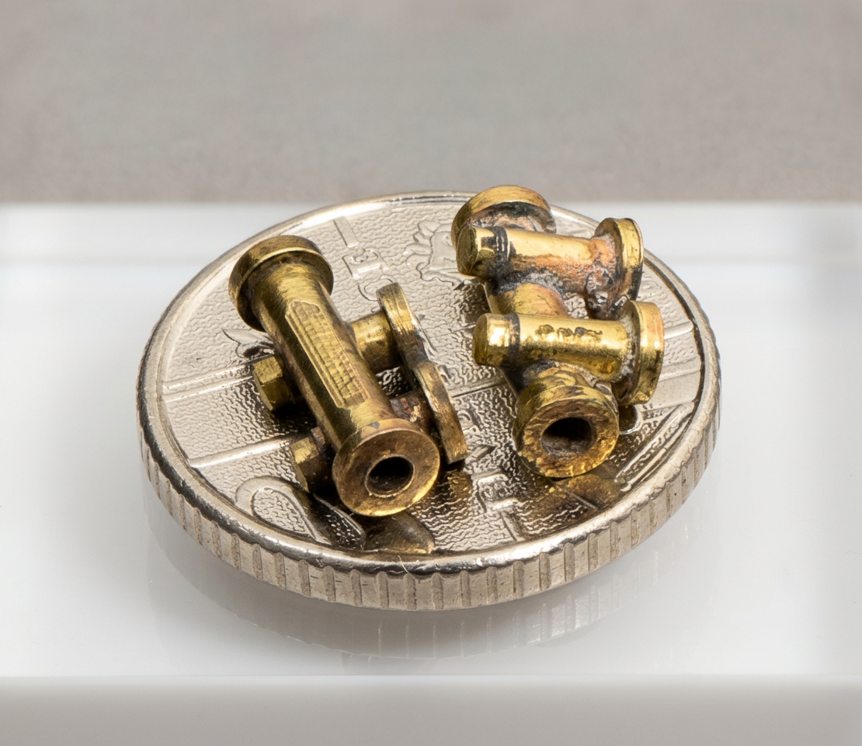
This is those parts assembled and again below after the AI treatment – It’s actually made them look quite pretty.
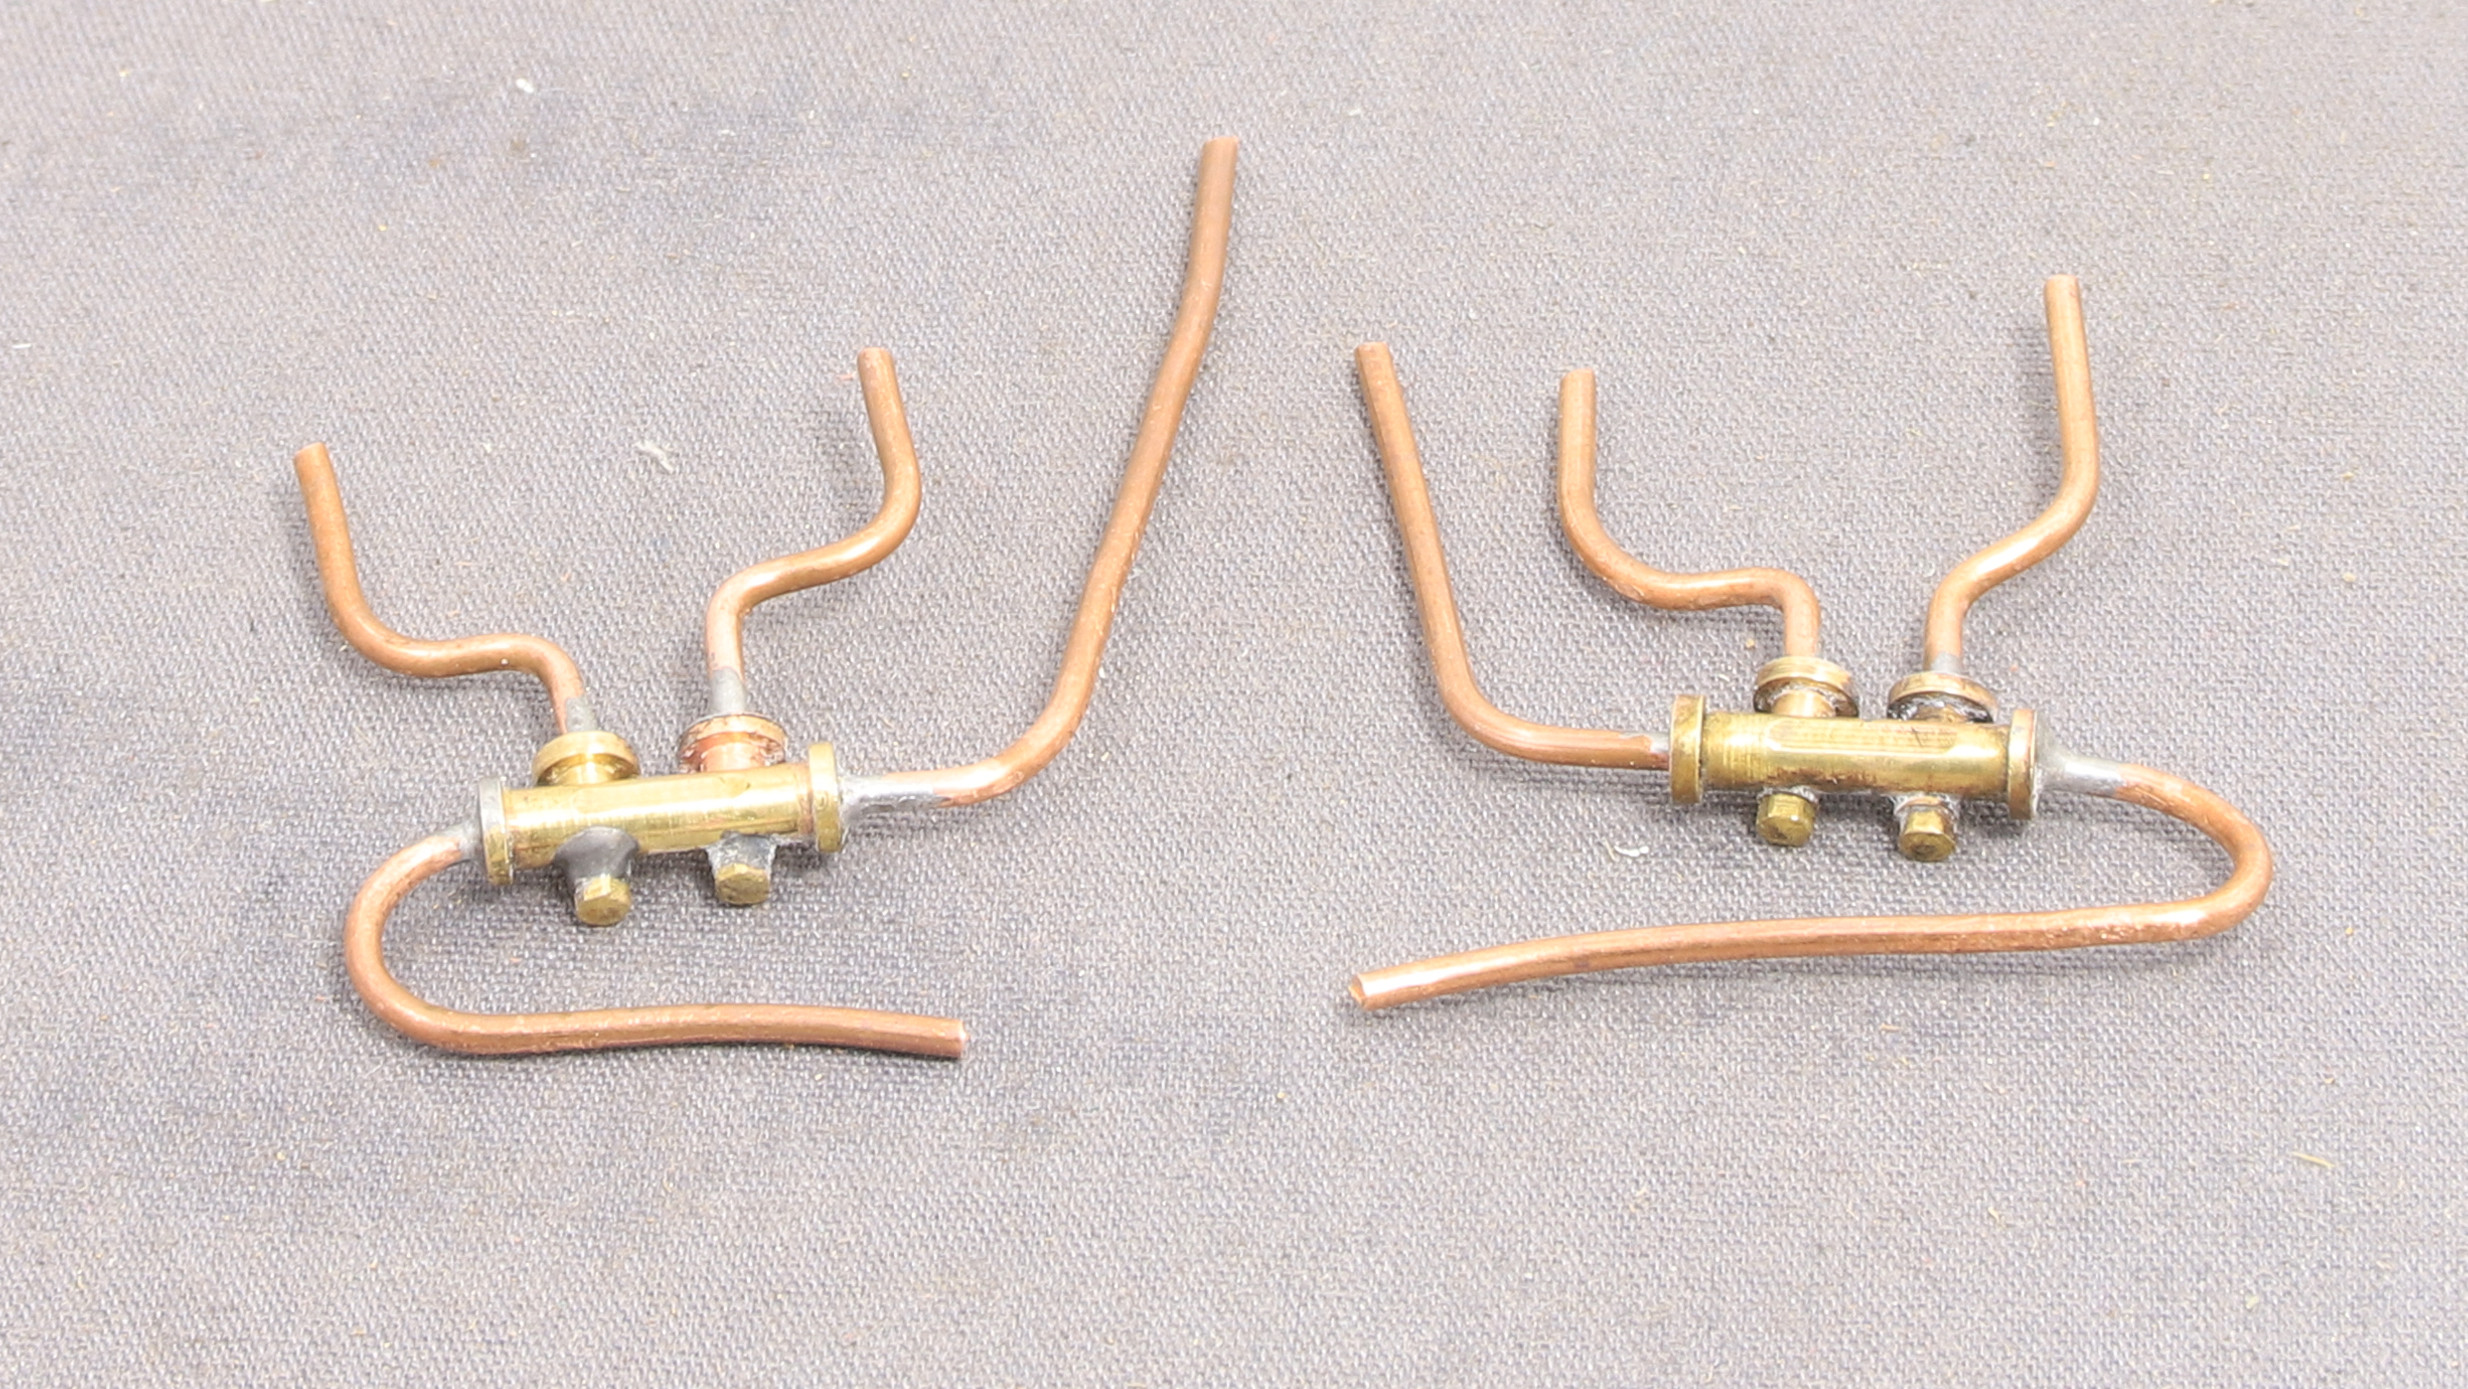
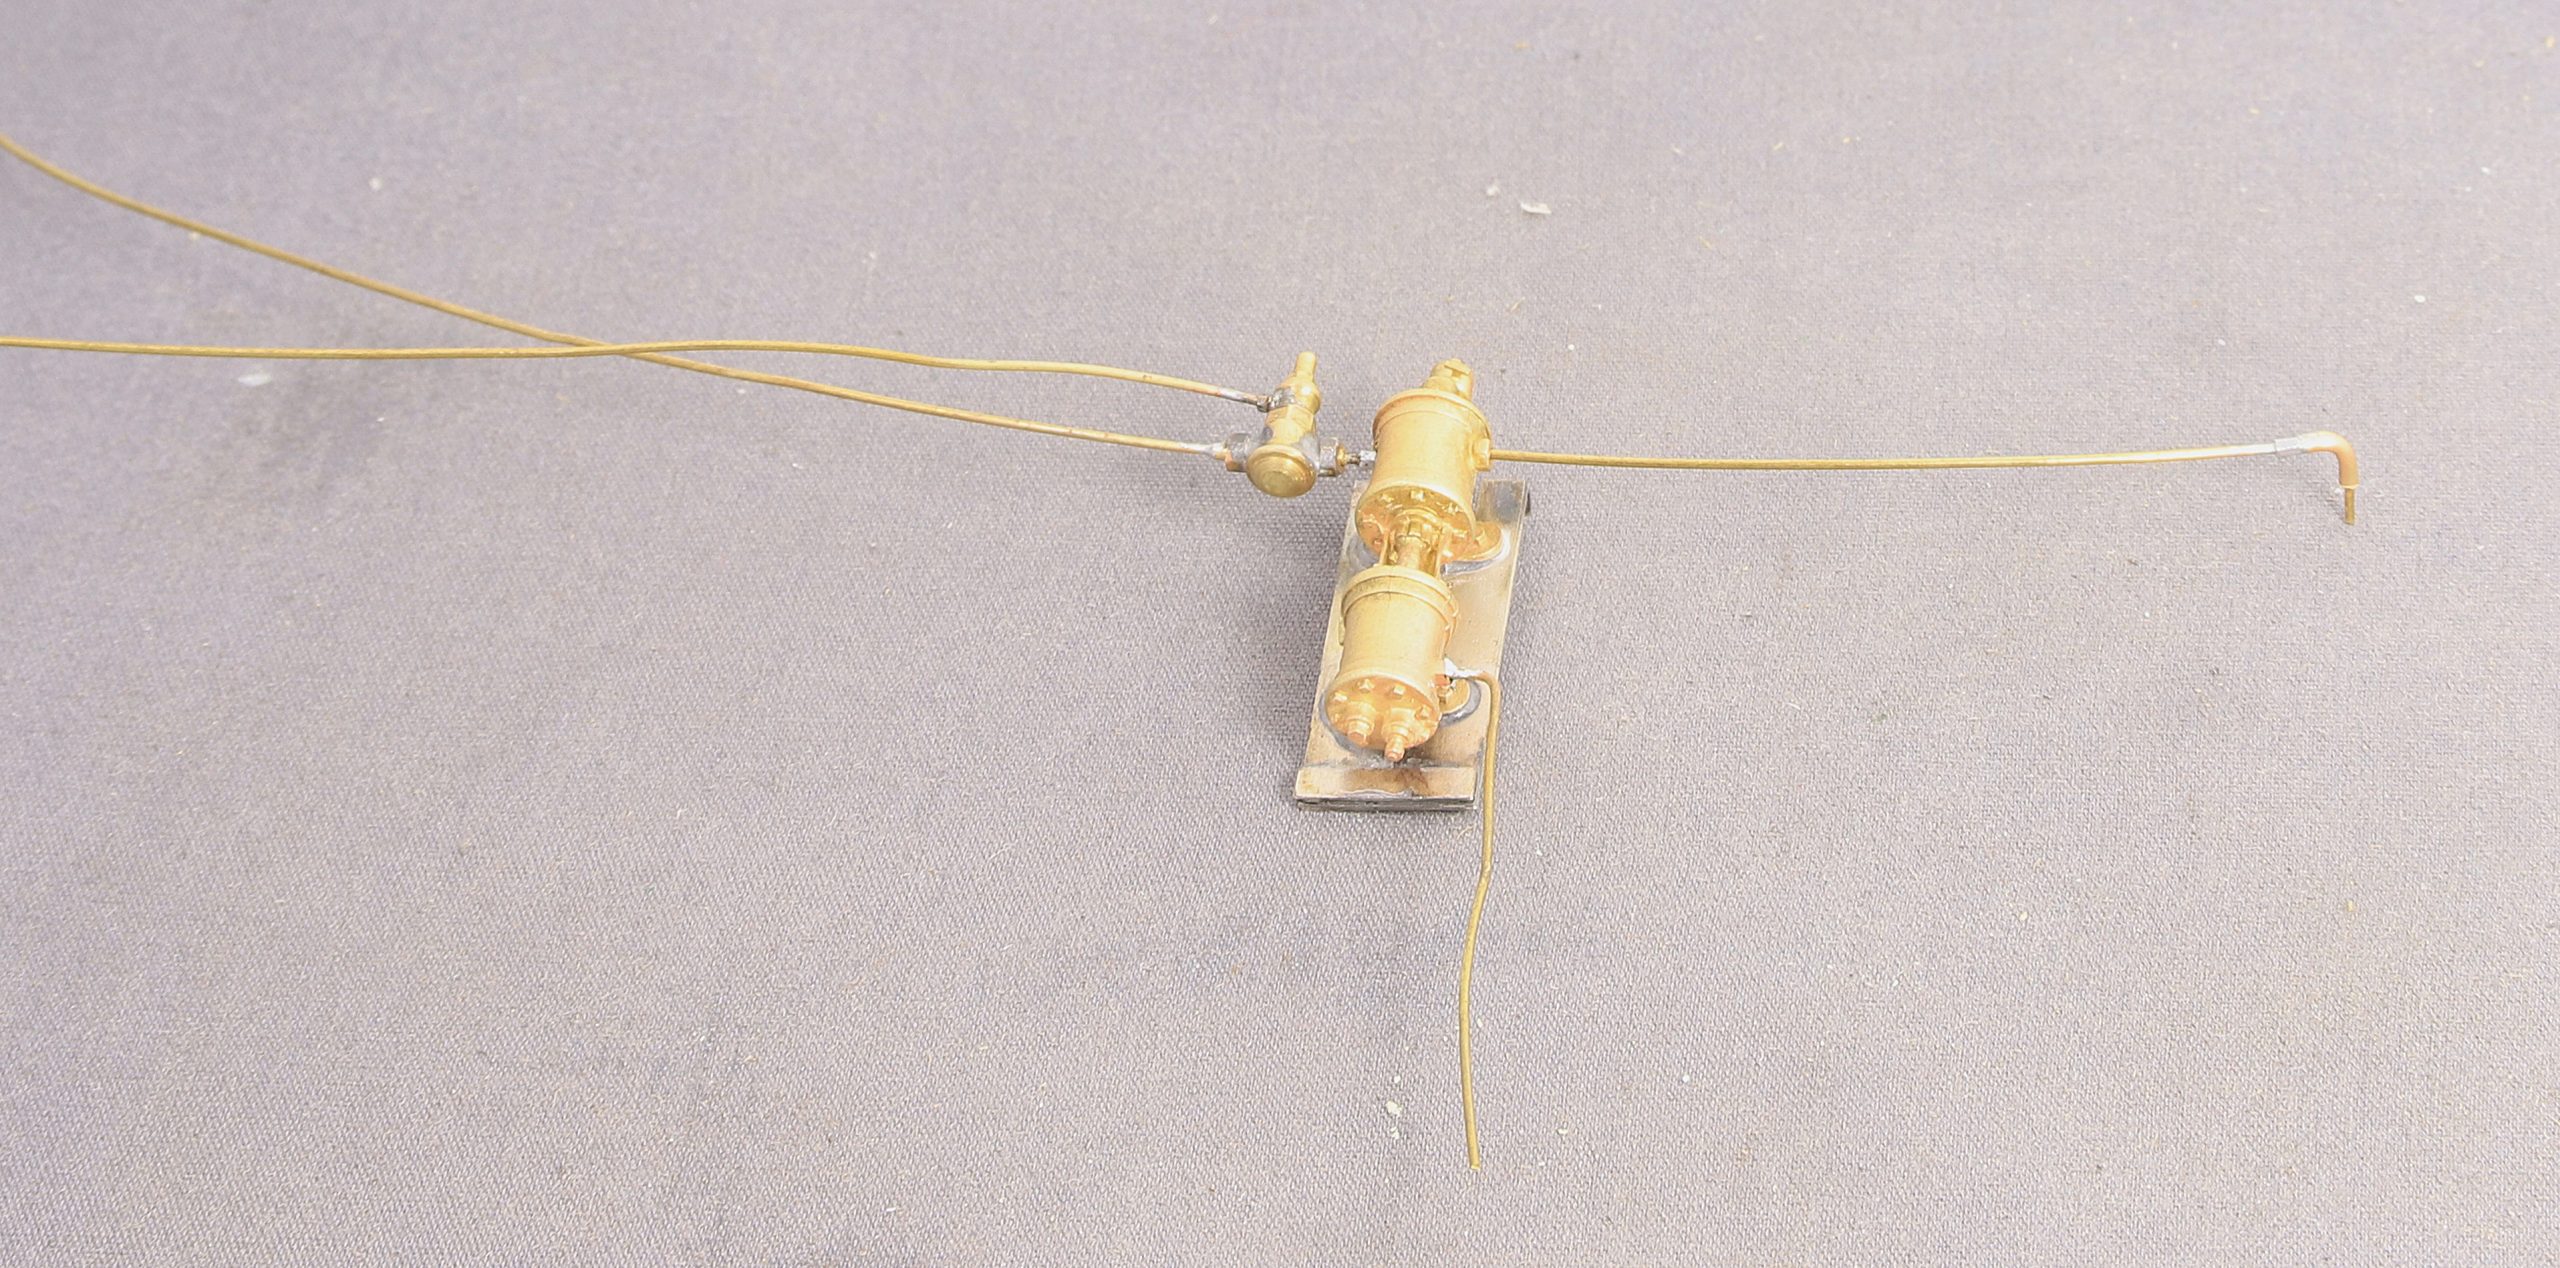
Finally for today I piped them up. It’s a shame that they will be almost completely hidden behind the steps
At our arts and crafts group last week I took along a length of rod to shape into the vacuum pipe that runs the length of the valance on the right hand side of the loco (a similar air pipe runs along the left hand valance). I only took the one length expecting it to take some time. As it happens I had it bent into shape in about five minutes so sepen the rest of the session talking to a friend.
Next on my list was balance pipes which fit behind the rear steps.
These were made to the dimensions of the GA and finished with some turned disks to represent the flanges.
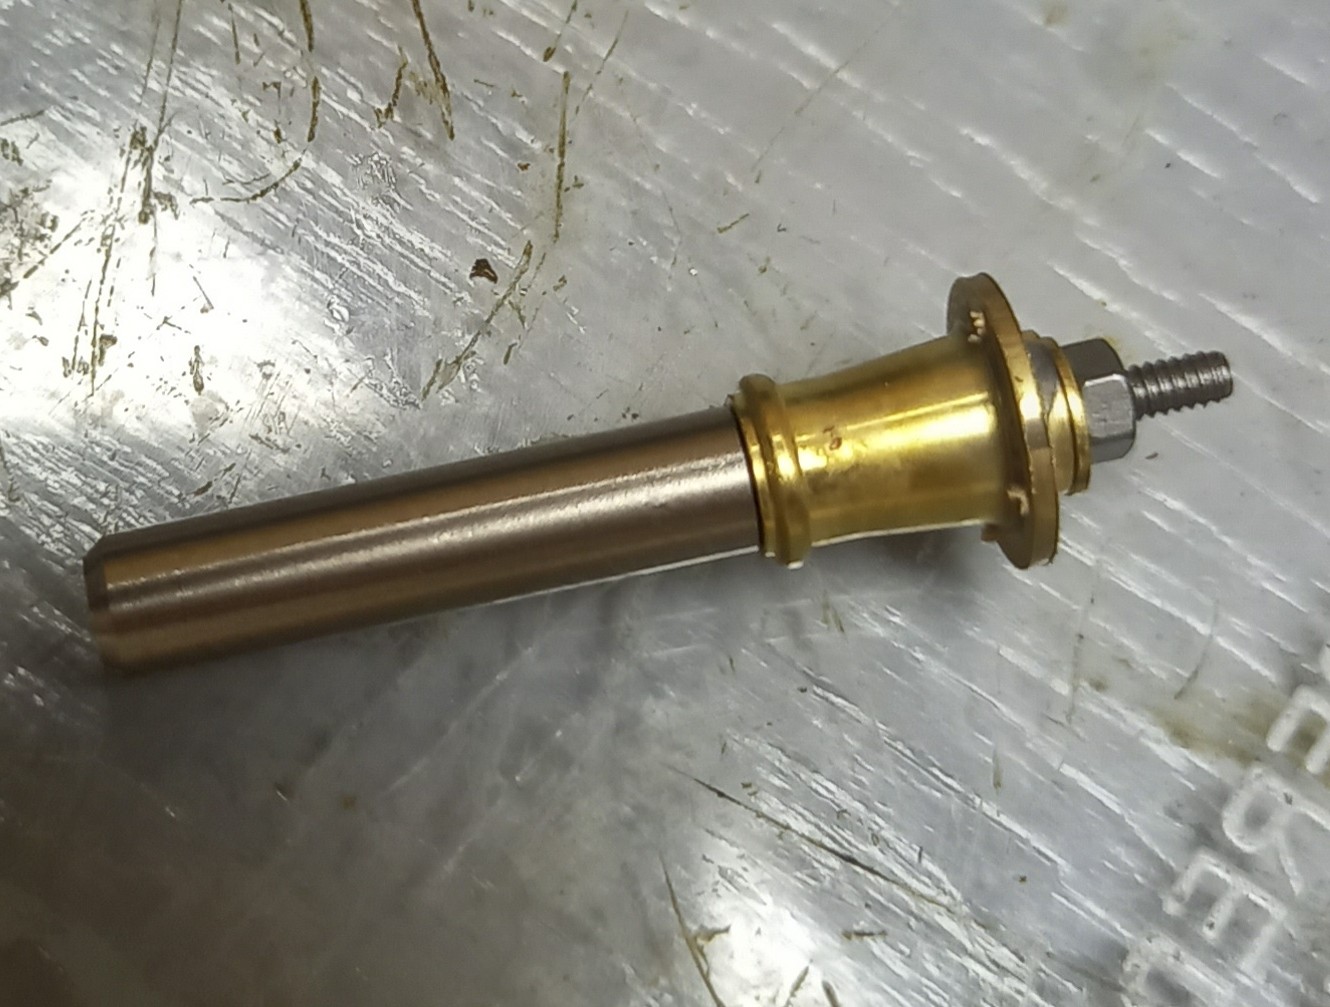
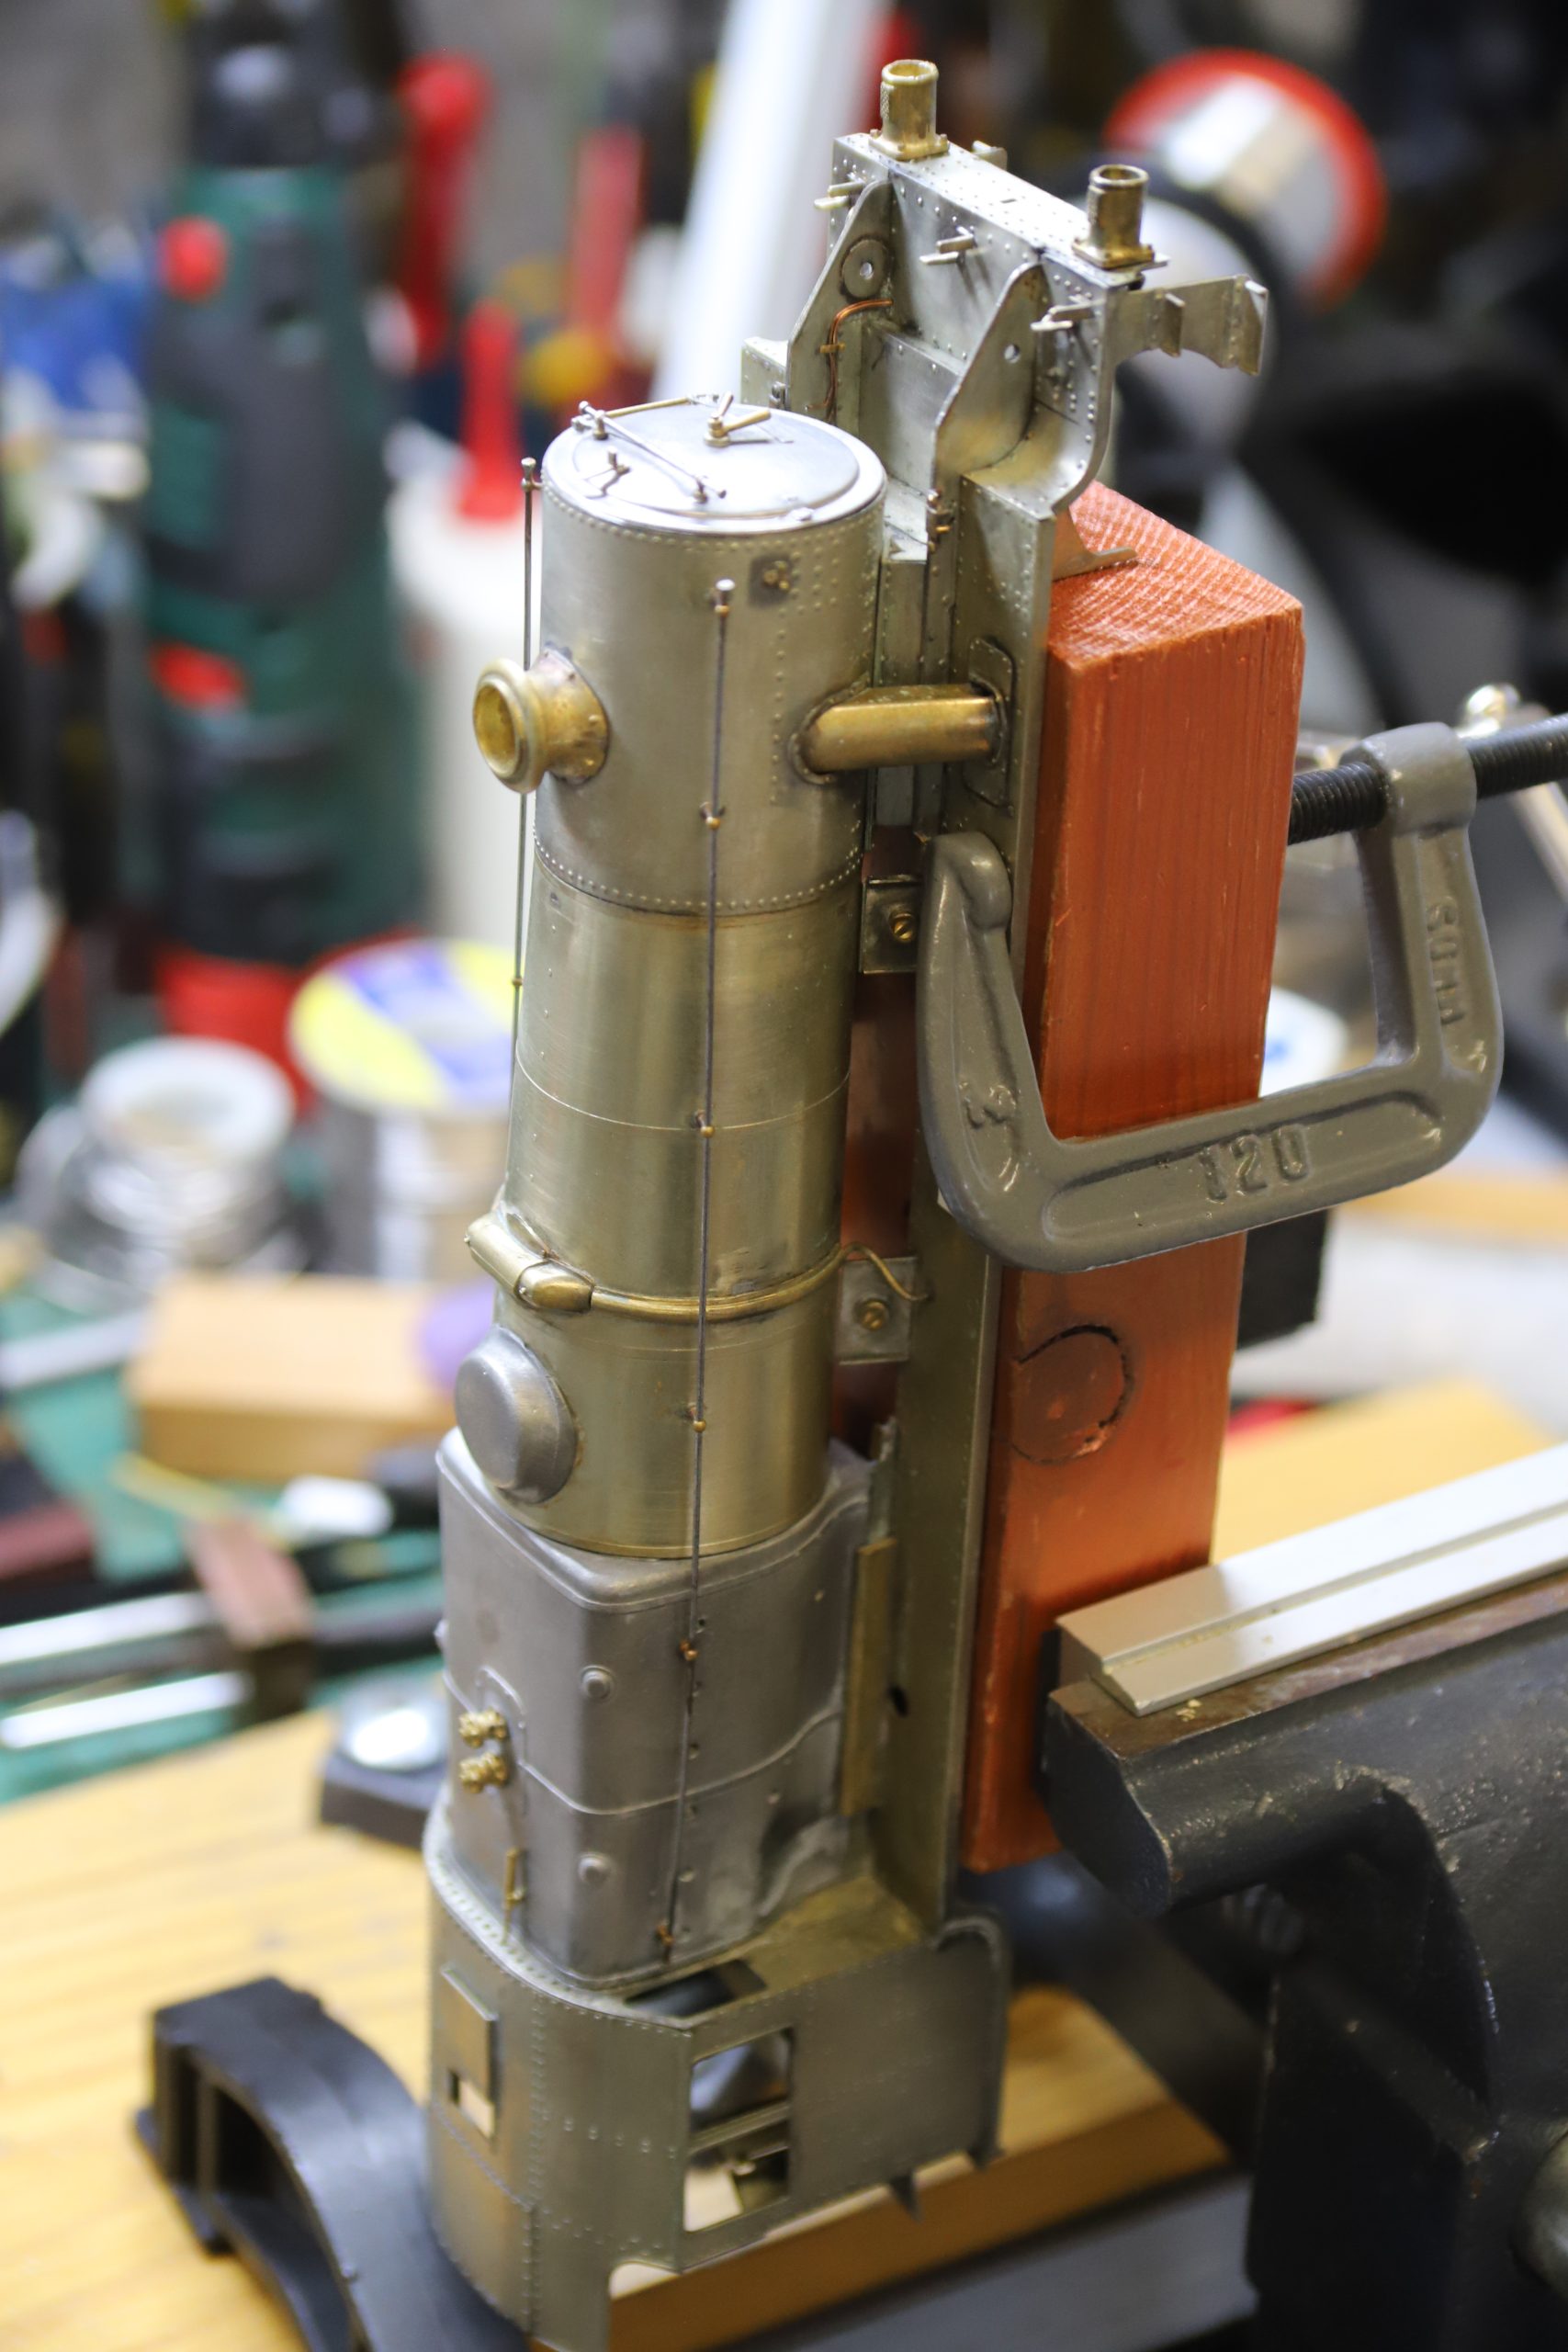
Next up was drilling out and fitting simulated bolt head to the buffer stocks. Due to the taper of the buffer stocks I figured it would be difficult to hold them securely without marking them and after some though I came up with an idea for a jig. The jig is made from 4mm steel bar recovered from a scrap printer, turned down to be a close fit in the major hole in the buffer stock and then threaded 10ba at the end.
This allowed the buffer stocks to be held upside down in my Proxxon dividing head to allow the drilling of holes for the simulated bolts.
There isn’t a lot of room for the bolt heads on the flanges of the buffer stocks so I needed something quite small. O opted to file som hex heads on some brass dressmakers pins but found that the smallest collet for my hex pin vice wouldn’t tighten down small enough to grip the pin shanks.
I’m not sure where it came from but in my tools I have a very small pin chuck which I believe is designed to hold very small drills in a bigger chuck on the lathe
After digging it out and pondering how I might index it I wondered if the thread was metric and by good fortune the very first nut that I tried fit perfectly (M5) this meant that I was able to tighten the pin chuck to grip the shank and then tighten the nut against the back of the collar to allow each facet to be indexed
After soldering the simulated nuts in place. I was able to use the little jig again to hold the buffer stock while I cleaned up the back of the protruding pins up in the lathe.
The last couple of workbench sessions have been preparing items for fitting.
I had done the rear steps some time ago but I hadn’t curved the treads. I did the front ones and curves all the treads at the same time.
Then I dug out the buffers. I’m not sure where they came from but I had secreted a set of NER buffers in the box some years ago. They came as a Buffer stock with a separate washer to create the rims that is bolted to the buffer plank. So they need to be soldered together. I also need to drill them and fit the prominent fixings that are visible in most photos
I also made a start on making the cab window frames so that they would open. I was fortunate that I had a spare set of etches for the wind frames so I soldered two together and then soldered a short length of microbore tube to the top so that I can hinge them
Lastly I machined a replacement upper rear lamp iron from the end of an earth pin out of the 13 amp plug
There is still quite a bit of the plug pin left for making other parts with at some point.
Westinghouse Pump and Governor fitted along with associated pipework. I’ve also fitted the vacuum ejector pipe and the Blower valve along with all the handrails at the front.
The next job was to make up the footplate, solebar and buffer beam unit.
The idea of the design is such that if you get everything correct then the footplate just clips into place. I added the solebars and frame spacers to the lower frame at a show. A subsequent test fit of the footplate at home, showed that I had one solebar slightly out of alignment so I had to take it off and reposition it.
Whereas this snip from a photo shows a curved cut out and flat ends to the buffer beam. I have a copy really old NER photo of no2 showing the same.
This is what the kit provides.
I spent the entire day at Thirsk show just carefully folding up the fold around edges for the buffer beams
At our arts and crafts group this week I added the final two stays to the 3D printed hand crane. It now needs a couple of bits of paint to touch up and the fitting of the chain/cord.
To that end while I was awaiting a visit from family today I knocked up a hook for the crane.
I also managed to progress the N10 a little further this week.
The first job was to drill out the Westinghouse casting. I have a couple of really nice brass castings in the stash which I believe are Alan Gibson but I’m not 100% sure. On the back of the mounting brackets there were a couple of spigots so I drilled a couple of corresponding holes in one side of a clothes peg and pressed the spigots into it giving me a secure grip when gripped in the drill press vice using another piece of clothes peg on the other side with a small parallel laid on it’s side to support them.
I drilled through the cast nuts on the right hand side then drilled a hole for the pipe that leads from the governor in the left hand side. While I ad the drill press out I also drilled the governor that I made for the last pipe and fitting.
lastly for now I assembled as much of it as I could prior ro fitting. In order to fit it to the etched mounting plate I cut and filed of the spigots on the mounting brackets and secured the casting to the bracket with 298 degree solder. Next I fitted the governor and the pipe that leads into the smokebox which is a little long at the minute and isn’t soldered in until I have it all mounted on the footplate.
On Thursday before leaving for Guildex on Friday I stuck the smokebox door onto the 8F. I had planned to do it earlier in the week but realised that the handrail wasn’t parallel to the hinge straps. I removed the handrail and moved one of the holes slightly before resoldering the handrail knobs back in. I also took the opportunity to add a small turned washer to the back of the smoke box door locking handles. I had neglected this detail when I added the handles at some time in the past.
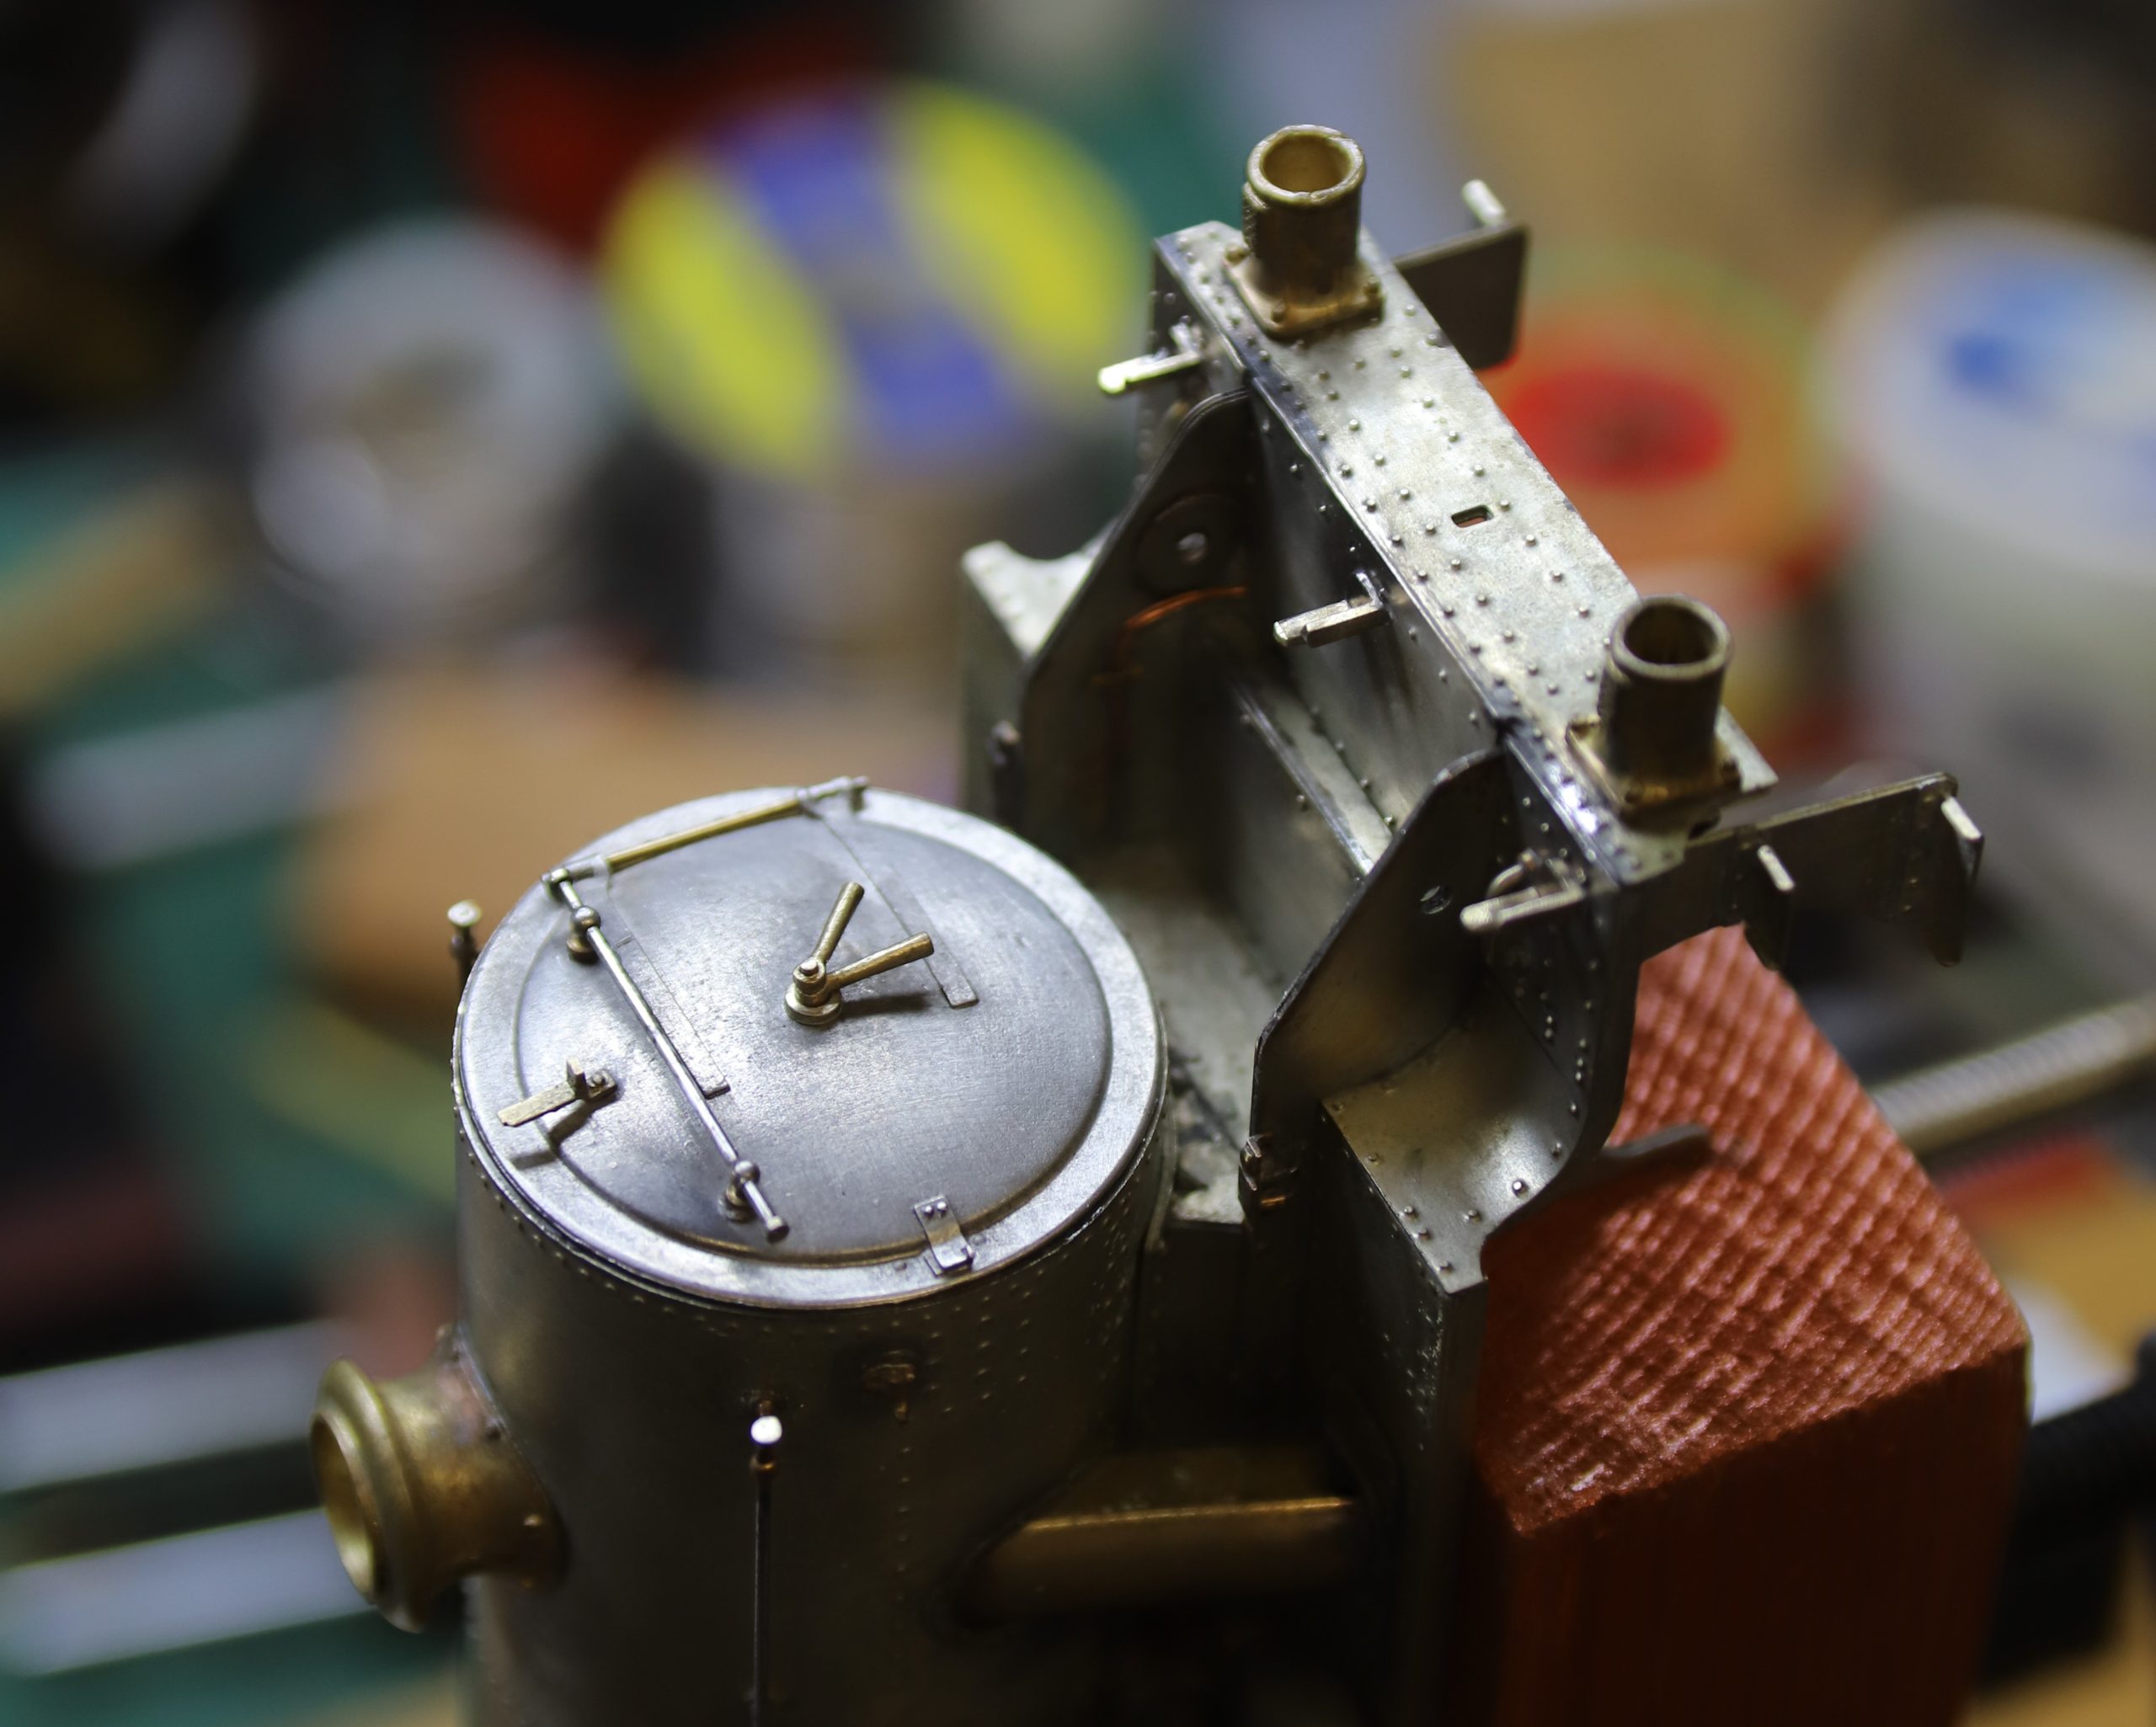
This is my rather Heath Robinson set up for holding the loco body vertically so that the epoxy didn’t allow it to slide out of position.
Those who dropped by the Technical stand on Sunday at Guildex were able to view both the 8F and the N10 in their current state, as I had them on the Sunday Display of members models.
Although the next logical step would have been to fit the brake shoes, I didn’t do that. I moved onto the cross beams instead.
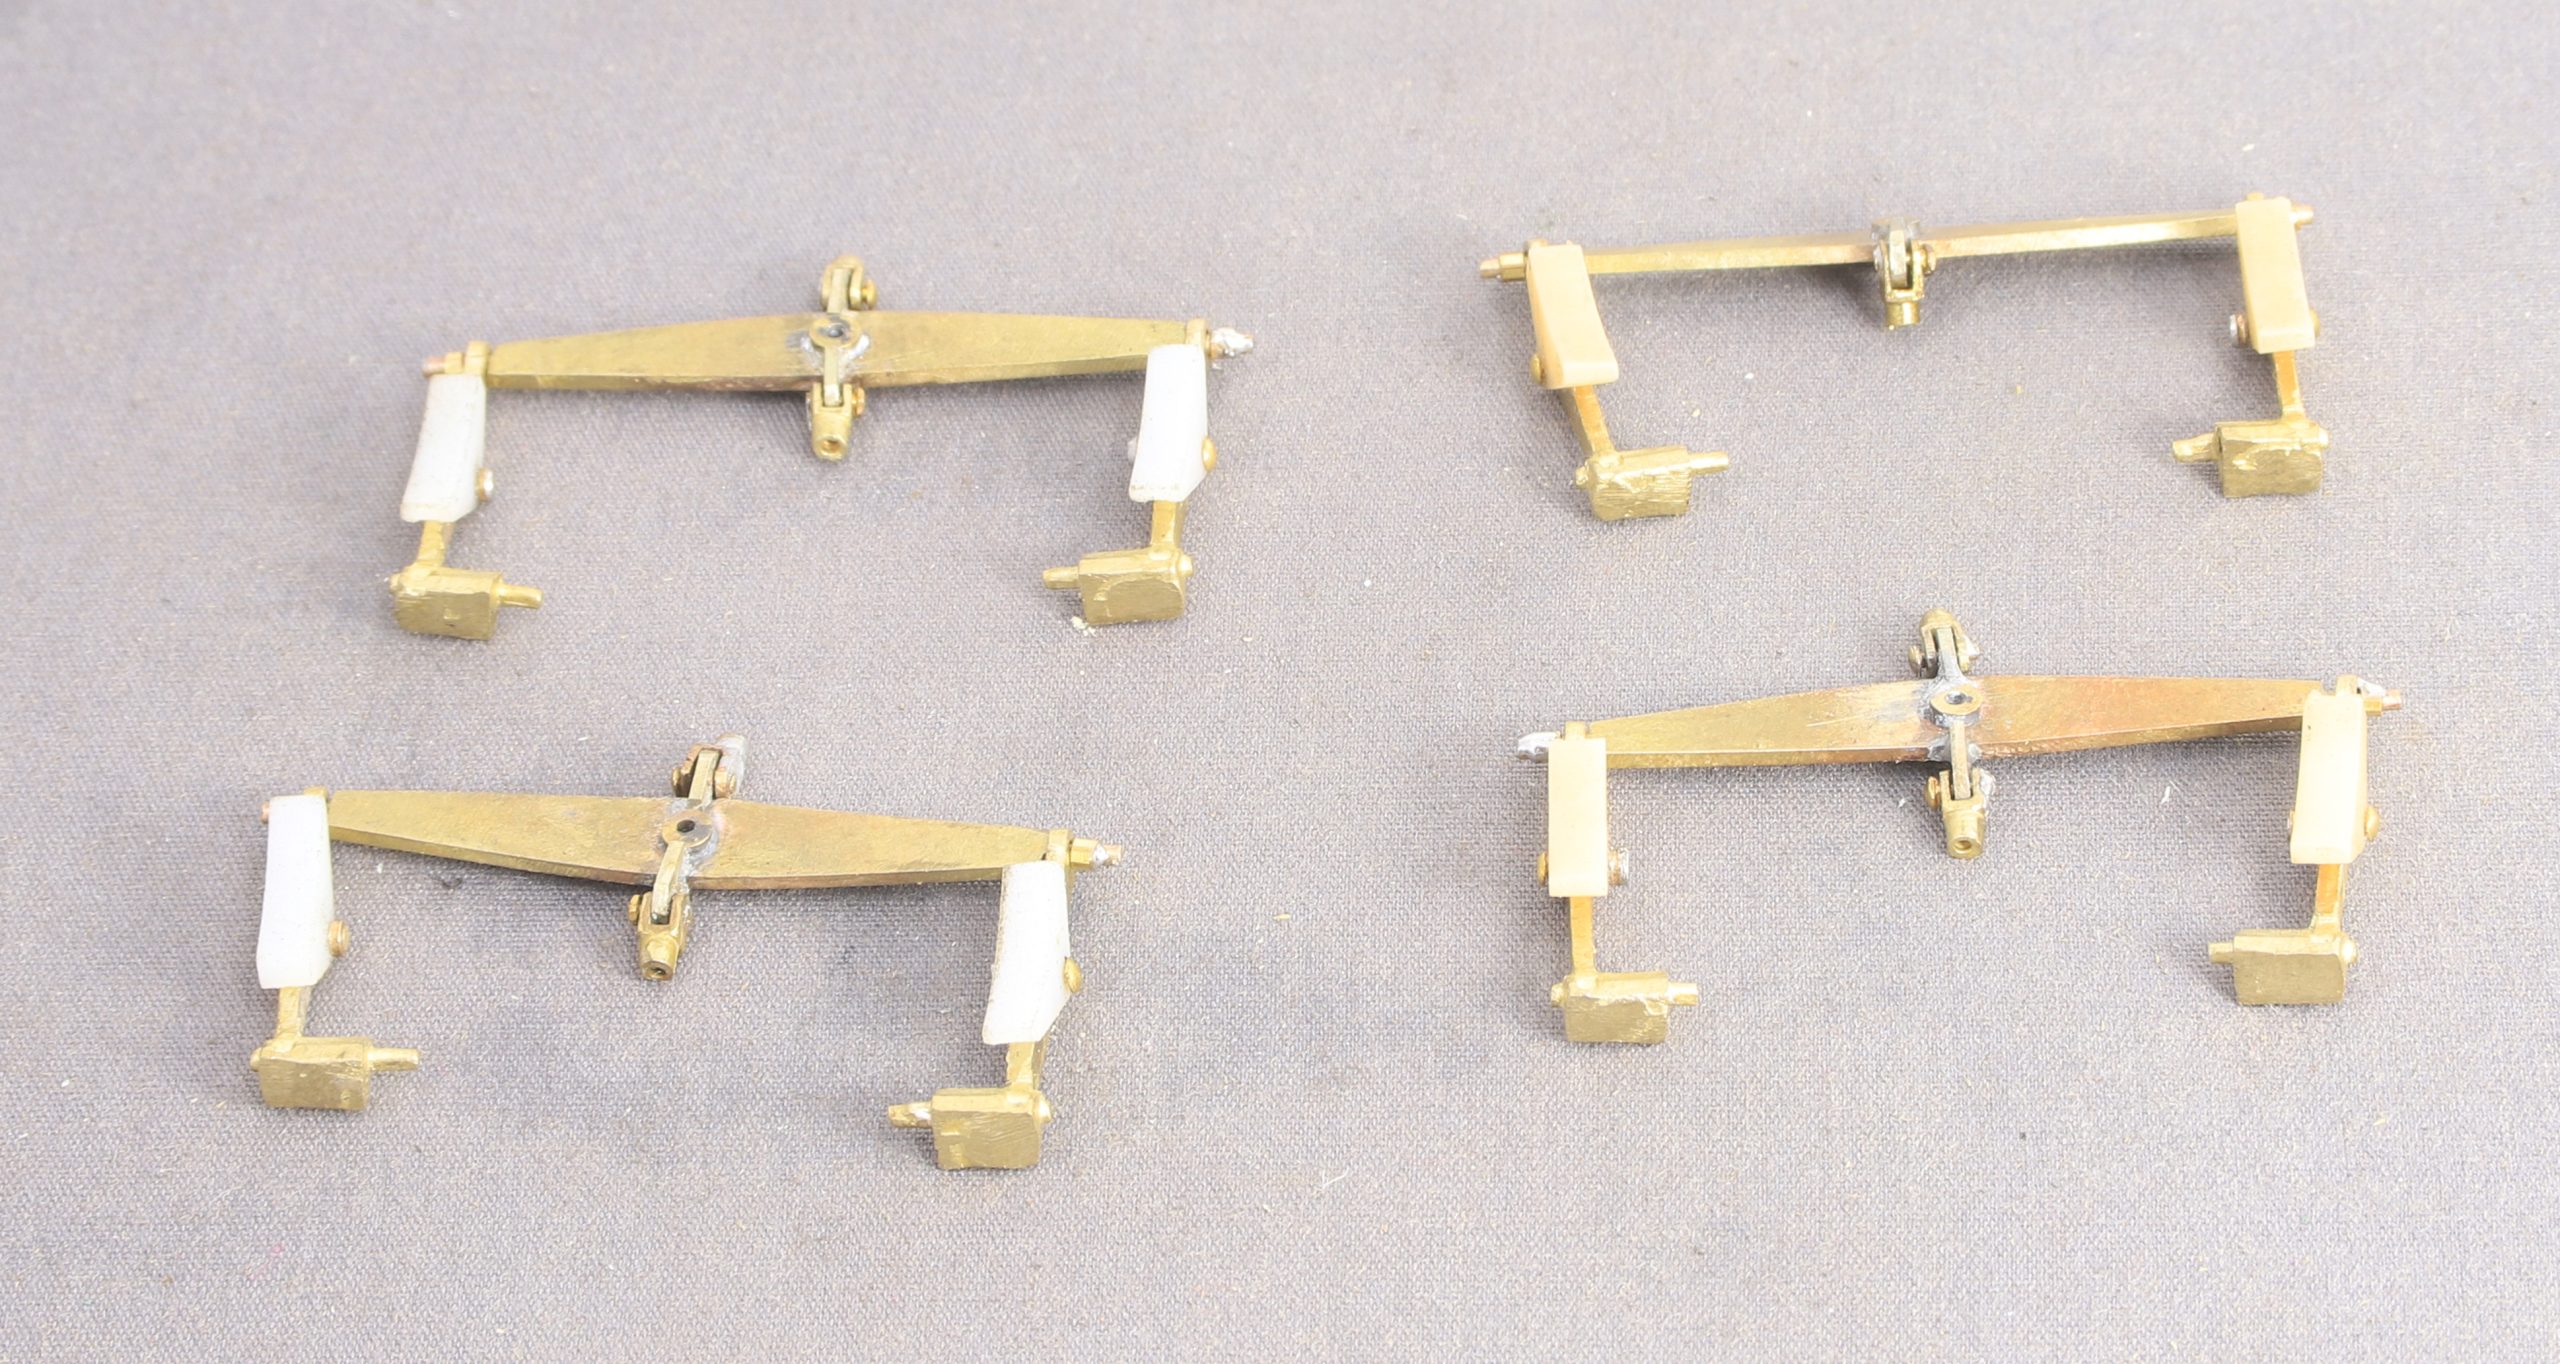
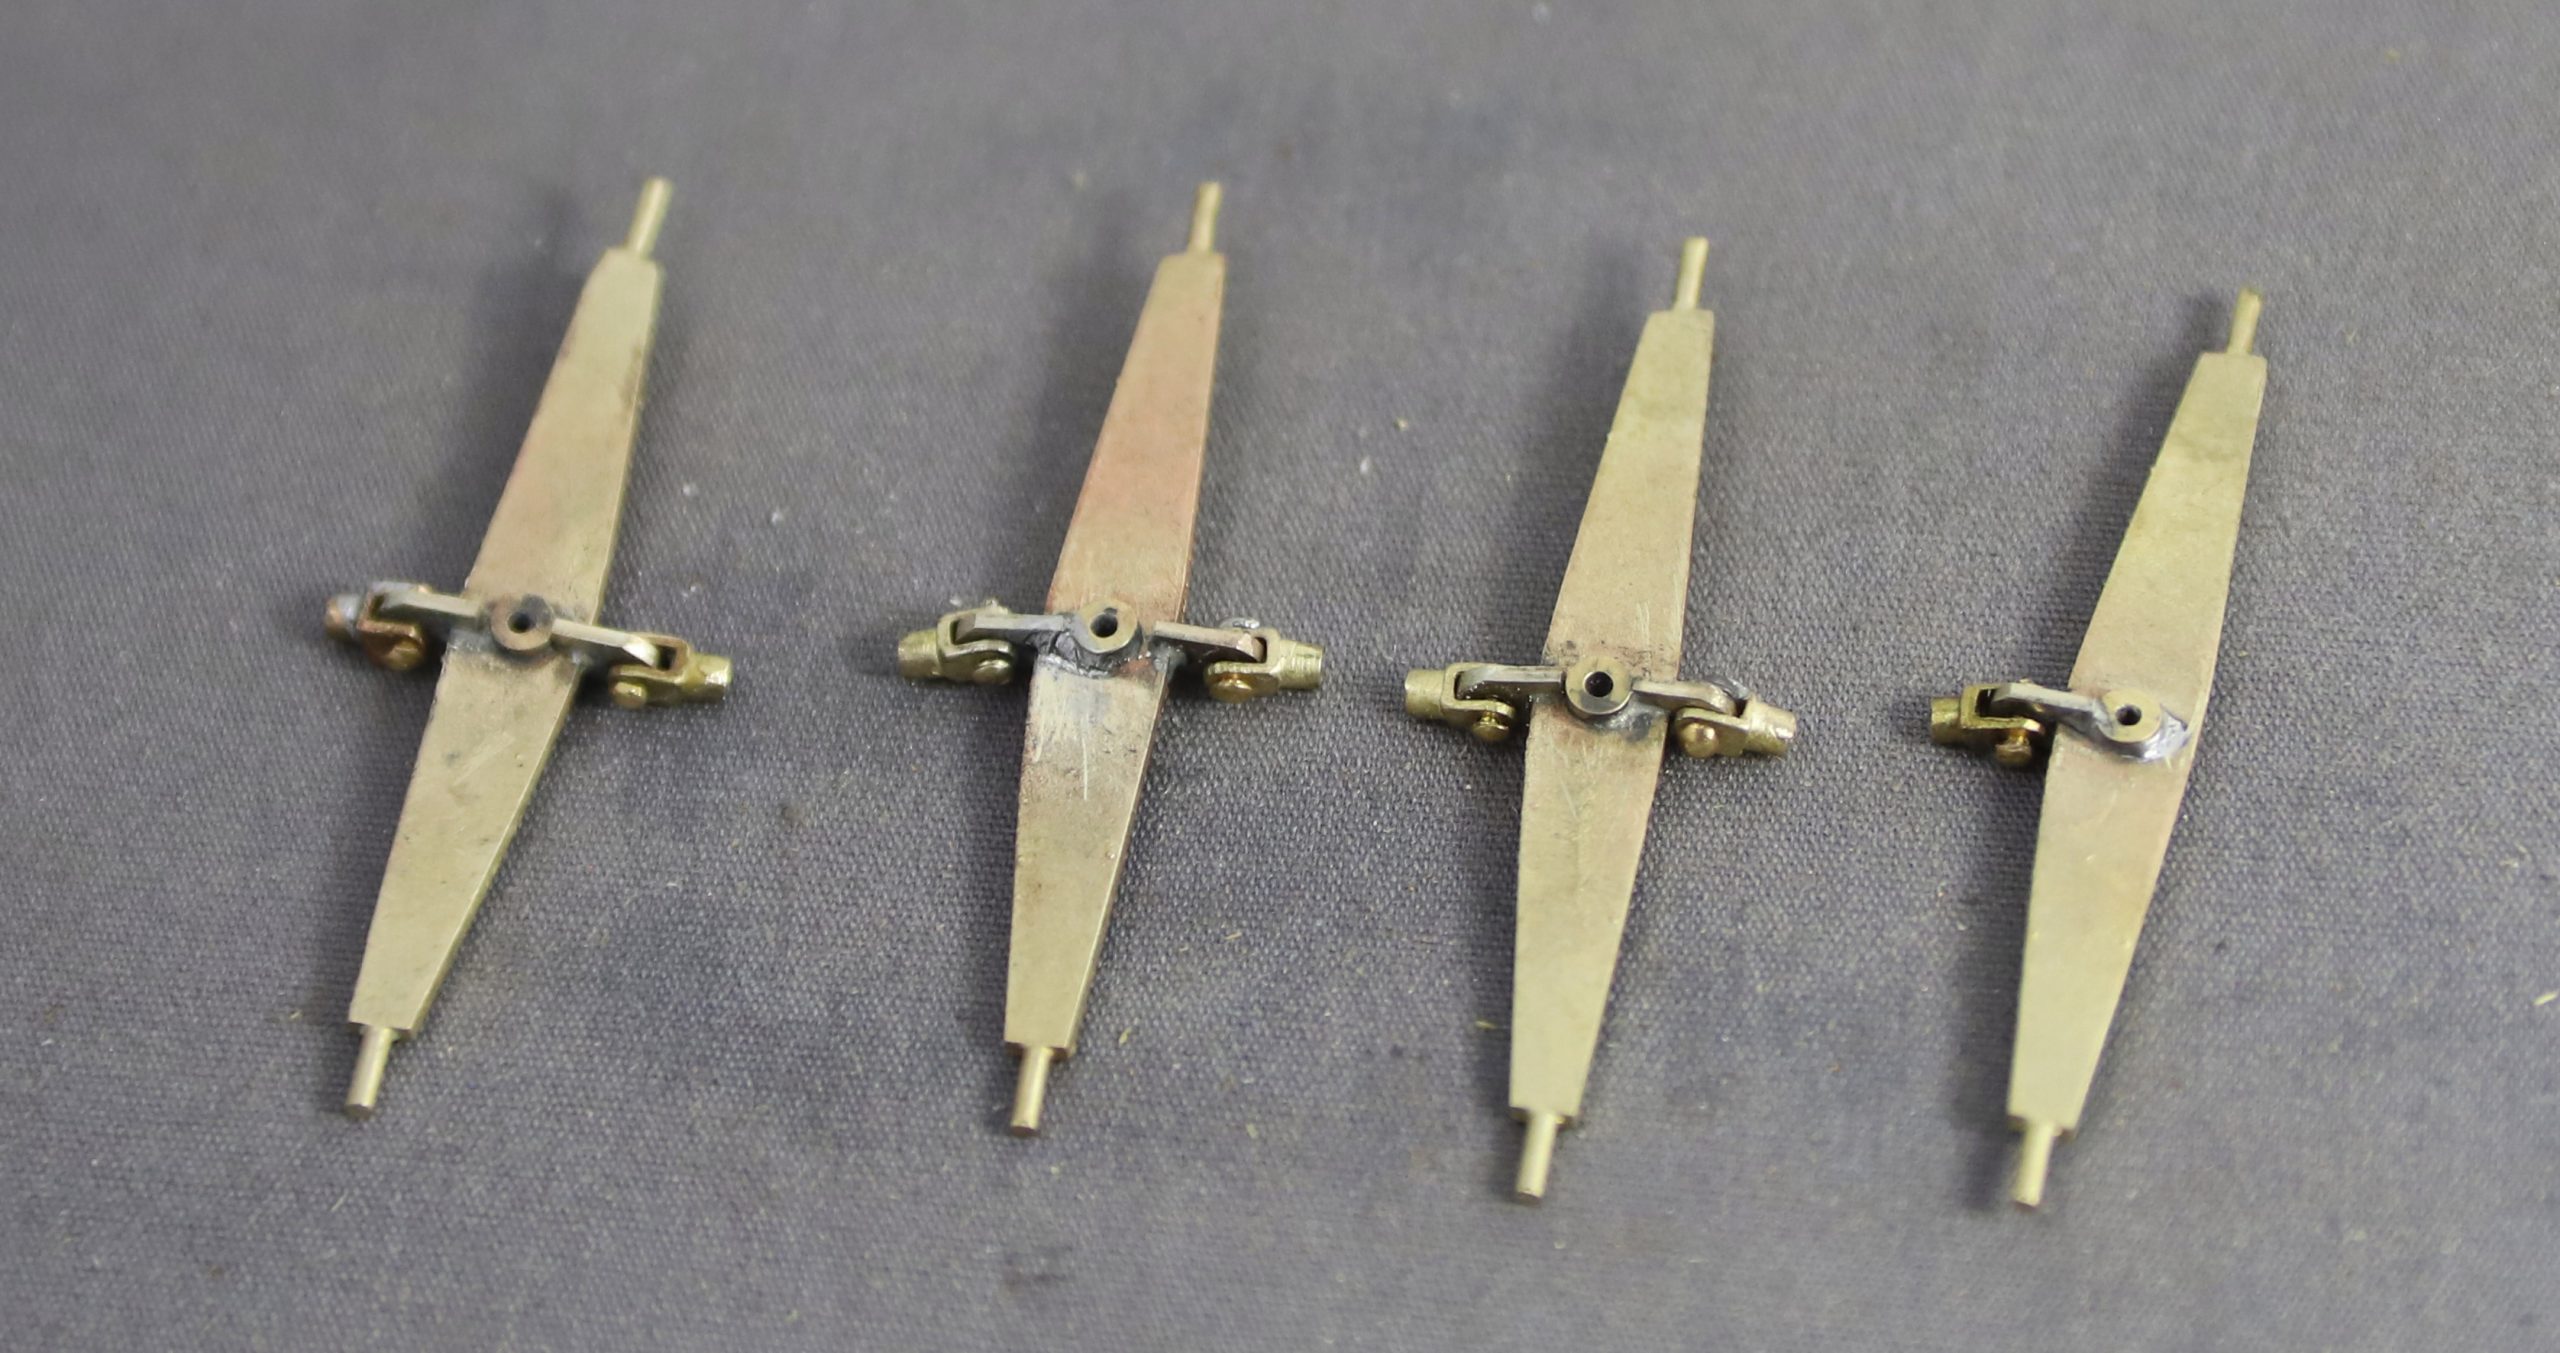
As supplied, they are flat castings tapering from the middle with pins asct in at either end. They also had a hole in the middle. While nice castings they are a bit generic and some time ago a fellow member of Western Thunder sent me some 3D printed brake shoes and some thick washers to beef up the centres of the beams along with instructions on how he had created his linkages.
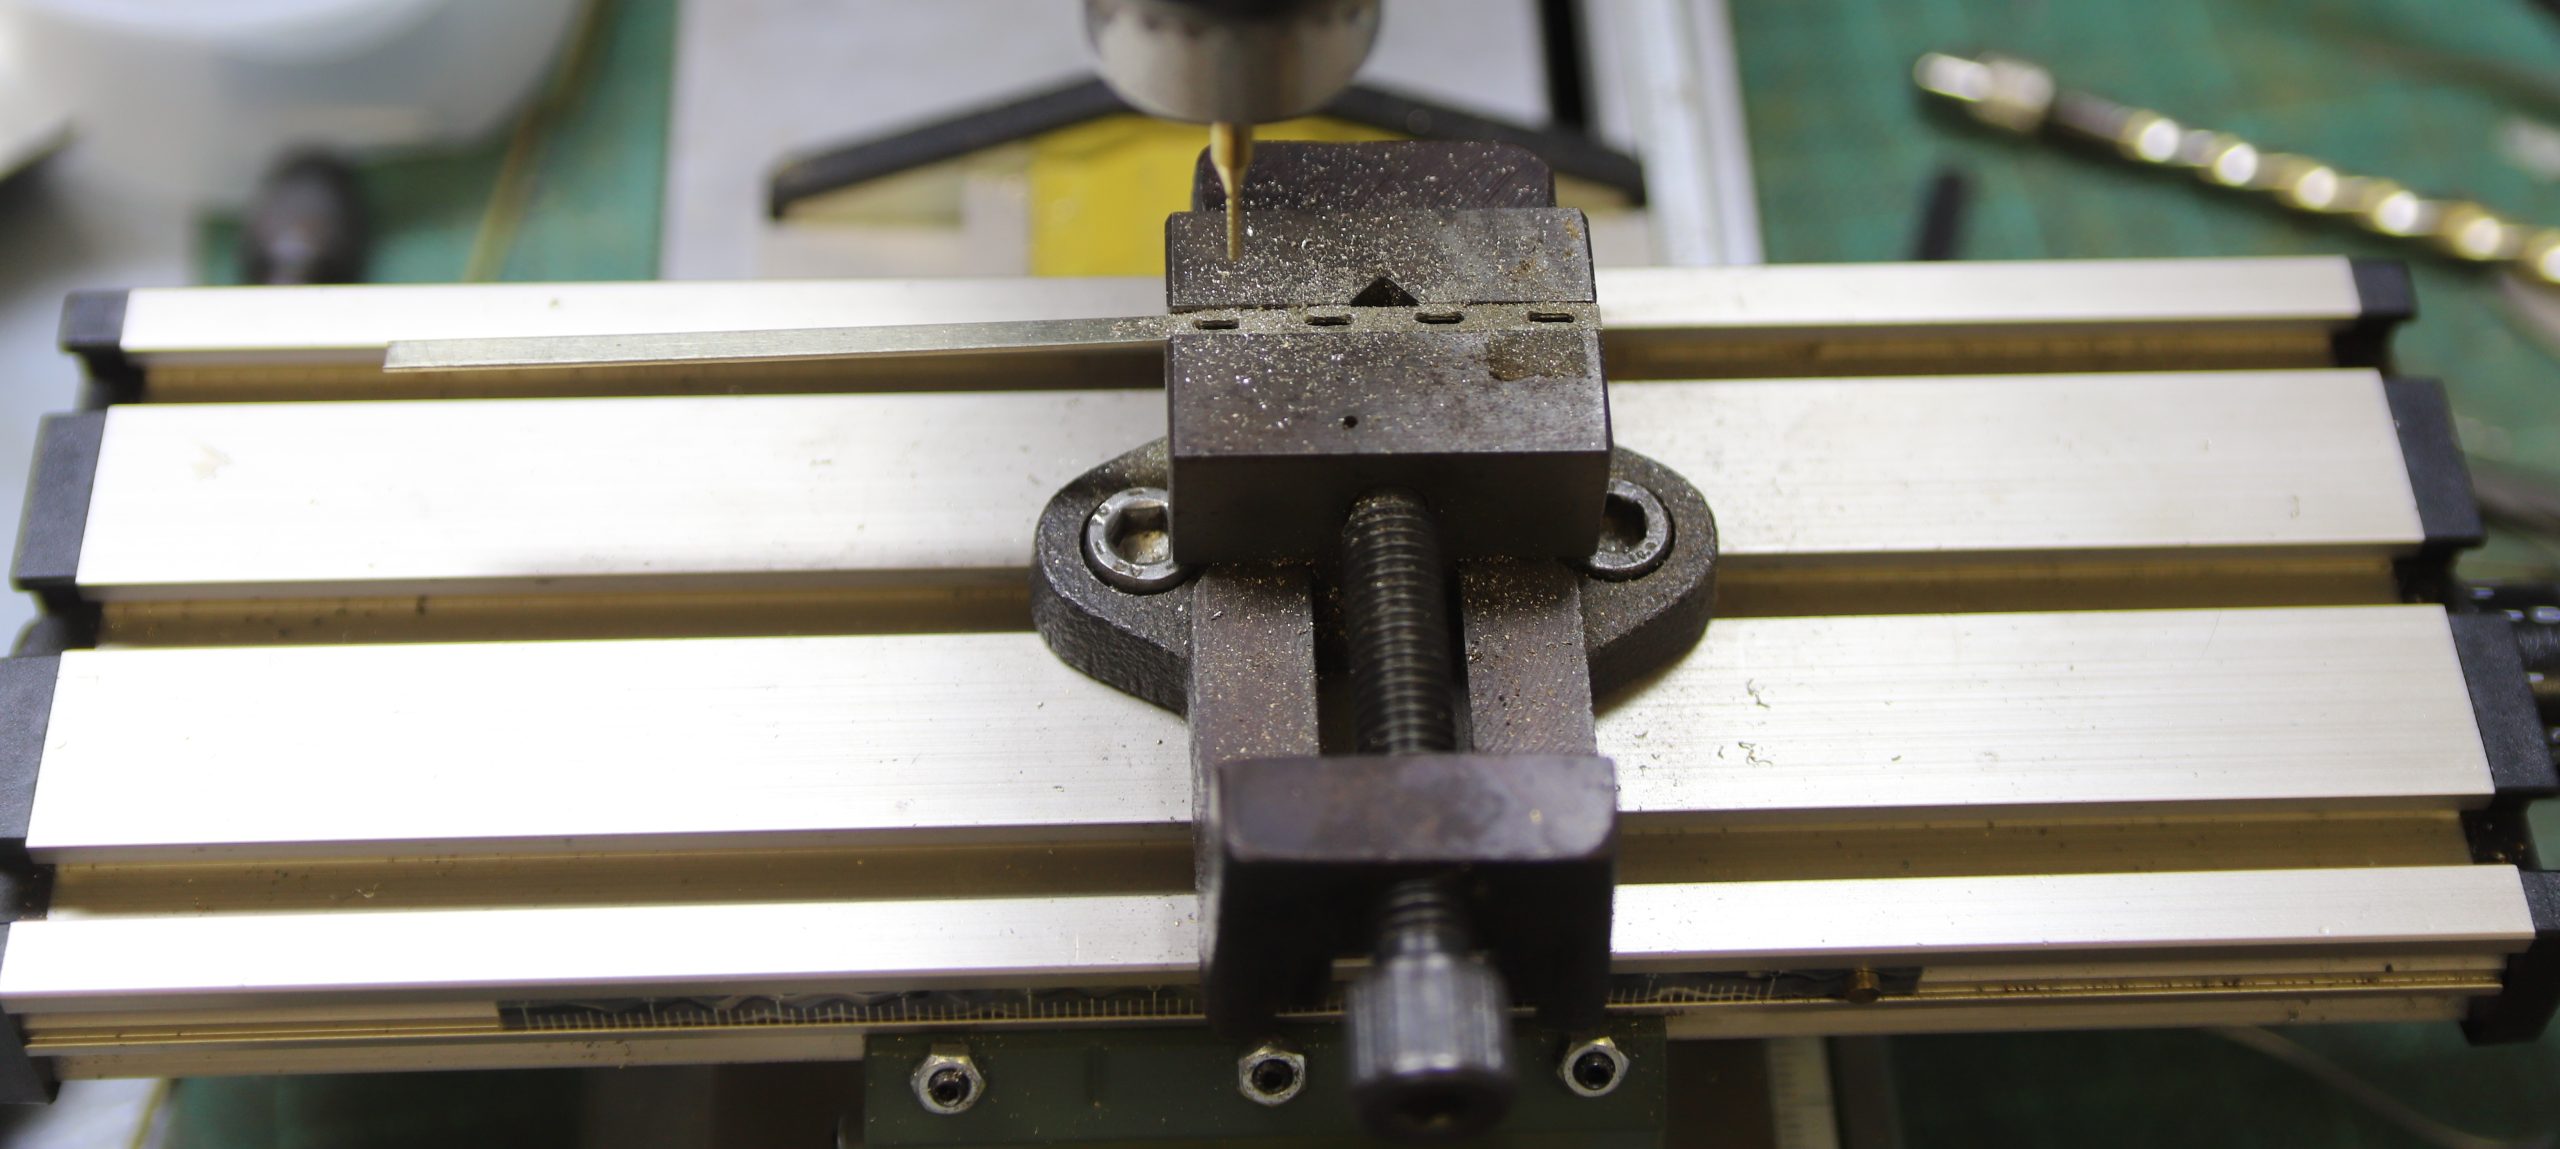
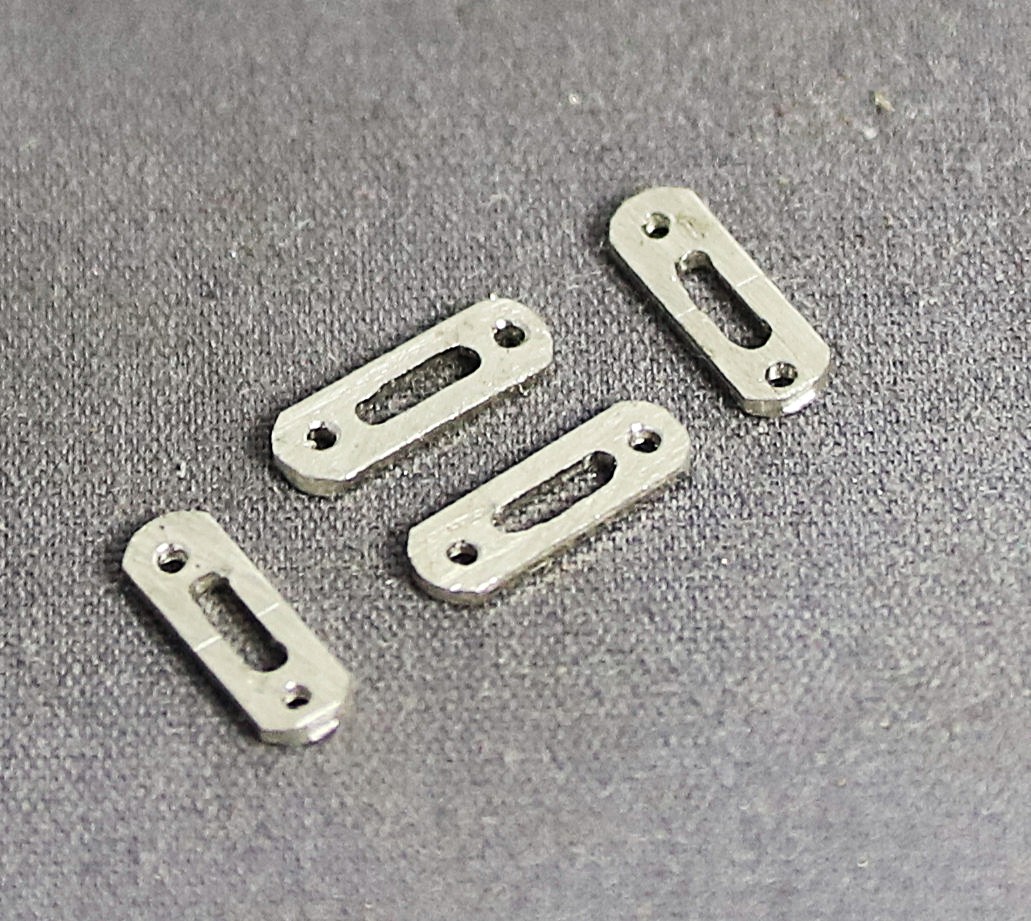
I started by cutting off a strip of 0.7mm nickel and then I drilled a series of holes in the strip to create the holes for each clevis to attach and to mark the beginning and end of a slot. Then I used a 1mm mill drill that I had previously bought from Amazon and pecked away at the slot until I joined up the holes.
Once separated and the ends rounded over, I was left with these.
The plan being that these too would be split in two giving me a pair of linkages for each side of the beam.
Although in theory I had one extra as ever one pair of them pinged off into the ether as I was soldering them together but I got there in the end.
Finally, I added the clevises which were provided in the kit.
This week I seem to have done quite a bit of work without a great deal to show for it but that’s how modelling goes sometimes.
I wanted to replace the cast brass brake shoes with 3D printed ones to reduce the chances of shorting. This meant that I needed to either file or mill off the cast shoes from the hangers.
I started by making a small jig to hold the hangers from another plug pin.
Machining Jig made from a Plug Pin
Before starting to mill off the brake shoes I first filed down the cast pivot pin and drilled a hole.
Then I milled off each side of the shoes
Then finally I gripped them edge on and milled away the final remains of the shoes.
Just to finish off the Westinghouse Governor discussion (for my part), on Tuesday our electricity was off most of the day (due to some planned work in the village).
Hence, after doing a few jobs outside, I was at a bit of a loss as to what to do next because I can’t see in the workshop without lights, so that was off limits. But it came to me that I could use Fusion 360 offline and I could also run my laptop on battery.
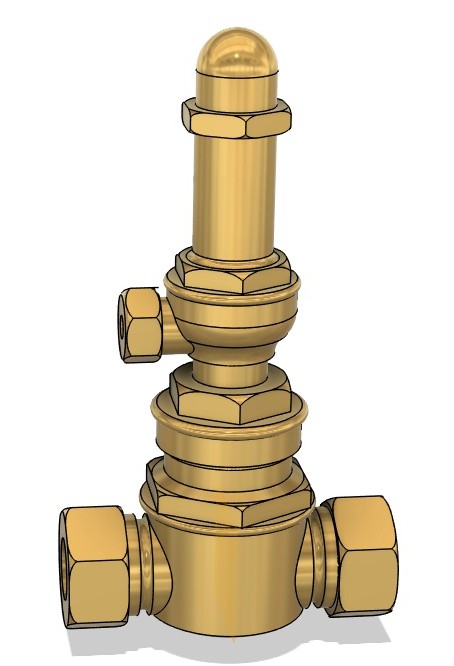
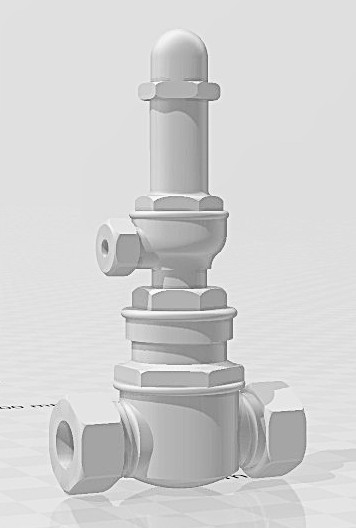
So I spent a couple of hours making my initial working sketches into a full 3d model of the Westinghouse Governor. Interestingly, I only used about 25% of the laptop’s battery charge in doing so.
I finished it off this morning but that consisted mainly of rounding off the edges of all the hex nuts.
The differences between this and my efforts with lathe and mill are clear, but given how small these things are in 7mm I’m still happy to use my analogue effort on the N10.
I need to remove my Spin Indexer from the mill to refit the vice to mill off the shoes from the brake hangers for the 8F. I plan to refit 3D printed brake shoes to the cast brass hangers.
So before spending time re-tramming the vice, I wanted to make sure that I didn’t need the spin indexer for anything else. Spoiler alert!, I did.
One thing that I have noticed in almost every photo of a loco fitted with a Westinghouse Pump, is that alongside the pump there is a Governor. You rarely see them modelled so I wanted to have a go. I did make one in the past for the Gladiator G5 but it only vaguely resembled the real thing.
As you can see from the 5p piece it’s a tiny little thing but I’m really quite pleased at how it’s turned out.
Although modelling has slowed down due to catching up with a few jobs around the house I have managed to do a bit more on the 8F.
I fitted the whistle albeit it still needs a drop of glue to secure it. Which I plan to do when I stick the smokebox door on.
That was to be the next job but when I came to dry fit it, I realised that the inner ring inside the smokebox was set back too far for me to be able to use epoxy to secure it. I would have needed to use that much that it would have run out all over. So I decided to make a couple of spacers to reduce the gap.
I cut a couple of squares of scrap etch (some of my older kits had quite wide edge strips which I saved) and then trimmed the corners off. I then used thick superglue to stick them to the short piece of thick walled steel tube that I used to make the quarter round transition rings for the N10 boiler/smokebox joint. Once secure I carefully turned them to size, initially taking off 0.05mm at a time, then working my way up to 0.1mm once I was confident that it wasn’t going to ping off.
In the end I only needed one spacer so one will go in the spares box.
Next I refitted the fall plate which had come adrift while handling the body and then I turned my attention to the cab doors. Like many I do prefer to make the cab doors articulate if possible and I had been pondering how I might achieve this before actually looking at the etches that make up the doors. Having examined them and worked out how they go together, I was pleasantly surprised to see that articulation is built into the design. in the end it was just a matter of soldering the two faces of the doors together then securing a length of 0.5mm wire through the “hinges” by soldering it to a half etched recess in the back of the doors.